High-Demand Twin & Contract Bedroom Systems
Explore our factory-direct models engineered for global commercial compliance, hotel projects, and luxury residential wholesale.
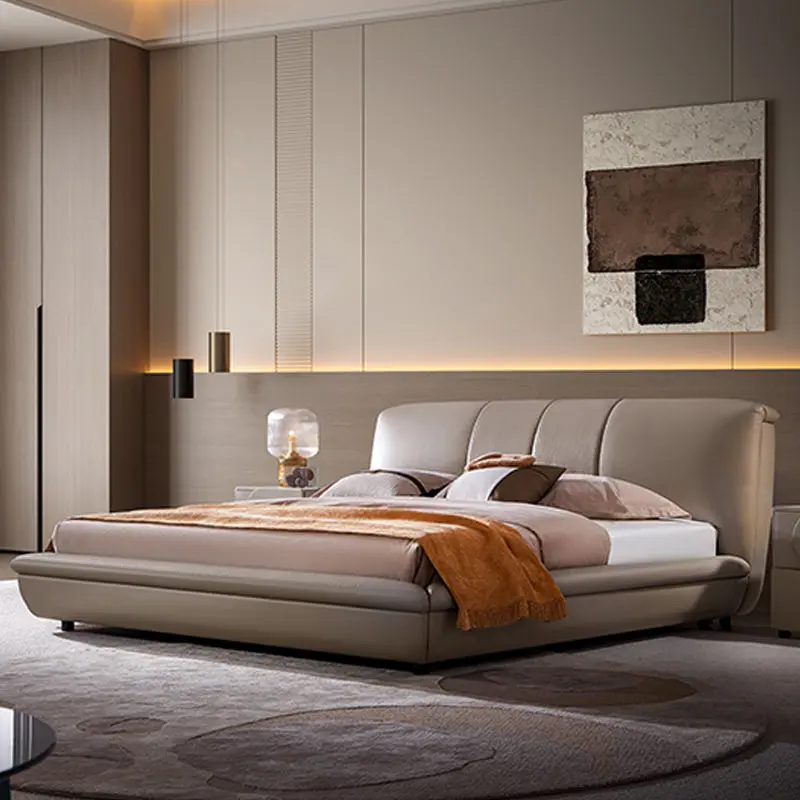
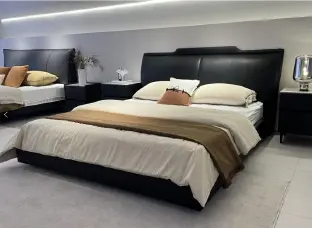
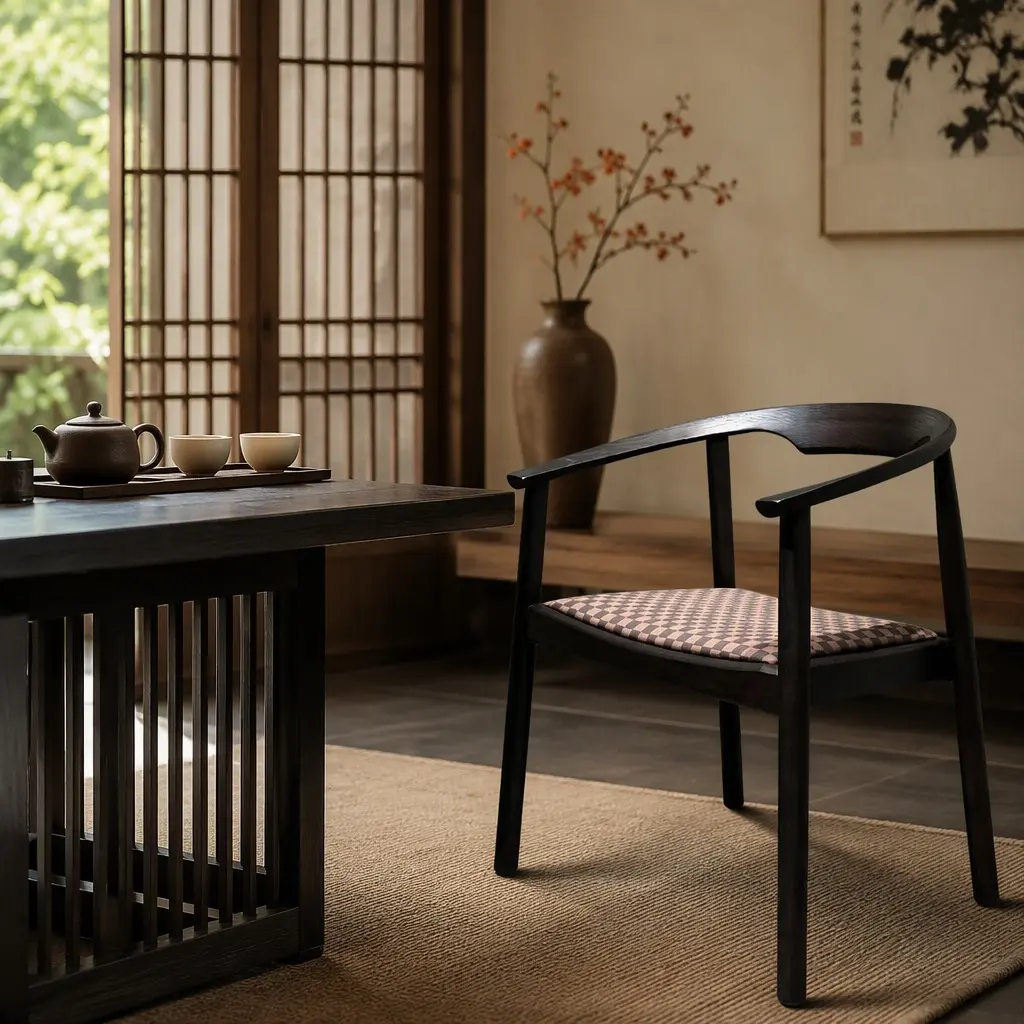
Twin Bedroom Furniture Evolution & Market Macro-Trends
The global twin bedroom furniture market is undergoing a seismic architectural transition driven by urban densification, the rapid expansion of international luxury hospitality brands, and the surge in co-living development. Historically classified as secondary residential items, twin beds, modular headboards, and space-optimized bedroom suites now represent core strategic assets for hotel chains, student housing operators, and furniture wholesalers worldwide.
As commercial real estate operators calculate yield per square meter, the demand for high-durability, multifunctional twin bedroom sets has escalated. Modern twin furniture engineering demands rigorous structural integrity to withstand intensive usage cycles in hotel environments, alongside customizable aesthetic profiles that fit contemporary Scandinavian, Italian Light Luxury, and Minimalist architectural themes.
China’s manufacturing ecosystem, centered in Foshan and Shunde (Guangdong Province), has redefined twin bedroom production through advanced Industry 4.0 integration. Overseas procurement teams no longer choose between cost efficiency and build quality. Chinese manufacturers now deliver structural joinery backed by solid wood internal cores, E0-grade eco-friendly emissions, zero-VOC surface coatings, and fire-retardant contract upholstery compliant with UK (BS 5852) and US (CAL 117) standards.
Global Enterprise Purchasing Metrics & Material Engineering
Understanding the engineering criteria that separate consumer-grade retail furniture from commercial-grade twin bedroom systems designed for multi-family and hotel deployments.
Structural Load & Framework Integrity
Enterprise buyers require twin bed frames tested to sustain static loads exceeding 400 kg to 500 kg. Leading Chinese factories utilize imported Russian Larch or solid White Ash internal cores, kiln-dried to a moisture content of 8-12% to prevent warping, cracking, or squeaking under dynamic load stress.
Advanced Material Surface Technology
From top-layer Italian aniline cowhide to ultra-breathable microfiber leathers and tech fabrics, modern factory applications include nano-scale stain-resistant coatings, moisture barrier backings, and high colorfastness ratings (> Grade 4.5) to withstand heavy commercial housekeeping protocols.
Logistical Load Density & Flat-Pack OEM
To combat volatile global ocean freight costs, Chinese OEMs engineer modular knock-down (KD) twin bed frames and flat-pack nightstands. Precision mortise-and-tenon structural fittings combined with steel cam-lock connectors optimize 40HQ container load volumes by up to 35% without sacrificing assembly speed.
| Specification Parameter | Residential Grade (Retail) | Commercial Hospitality Grade (China Factory OEM) | Testing & Compliance Standards |
|---|---|---|---|
| Internal Frame Timber | Softwood / MDF Boards | Kiln-Dried Russian Larch / Solid White Ash Core | FSC / ASTM D4442 (8-12% Moisture) |
| Cushioning Foam Density | 22 kg/m³ - 28 kg/m³ | 45 kg/m³ High-Resilience Virgin Foam + Latex Layer | ISO 845 / CertiPUR-US |
| Fabric Abrasion Resistance | 10,000 - 15,000 Rubs | 50,000 - 100,000+ Martindale / Wyzenbeek Rubs | ASTM D4966 / ISO 12947 |
| Fire Retardancy | Standard Consumer Grade | Flame-Retardant Upholstery & Foam | BS 5852 (Crib 5) / US CAL 117 |
| Formaldehyde Emission | E2 / Basic Standards | E0 / CARB Phase 2 / Ultra-Low VOC | EN 717-1 / EPA TSCA Title VI |
China Industry 4.0: Supply Chain Resilience & Efficiency Advantage
The global competitiveness of China's twin bedroom furniture factories stems from decades of targeted cluster development, particularly within the Pearl River Delta industrial hub of Foshan and Shunde. Today's leading facilities have evolved from labor-intensive workshops into automated Industry 4.0 manufacturing eco-systems.
1. Hyper-Localized Supply Clusters
Within a 30-kilometer radius in Foshan, manufacturers have direct access to specialized suppliers for solid wood timber, precision hardware, high-resilience polyurethane foam, eco-leather tanneries, and export packaging facilities. This proximity reduces component lead times from weeks to hours.
2. Automated CNC Woodworking & Laser Cutting
Modern twin bed factories employ 5-axis CNC machining centers, automated timber sanding systems, and computerized leather nesting software. Precision component cutting ensures zero-tolerance fitting across large-scale commercial contract orders.
3. Rigorous Multi-Tier Quality Assurance
In-house laboratory testing rigs simulate real-world physical stress: 100,000-cycle mattress impact tests, corner drop tests, hardware salt-spray corrosion tests (48-hour rating), and climate-chamber stability trials for fluctuating humidity environments.
This integrated infrastructure allows Chinese manufacturers to offer customized OEM/ODM twin bedroom suites with production turnarounds of 25 to 35 days for full container loads (FCL), providing unmatched agility for international project buyers facing strict construction delivery deadlines.
Global Commercial & Industrial Application Scenarios
Tailoring twin bedroom furniture design and material engineering to match specific industry operational needs across worldwide markets.
High-Density Hospitality & Resort Suites
Requirement: Rapid room reconfiguration, high stain resistance, acoustic dampening.
Factory Solution: Modular twin bed frames equipped with hidden heavy-duty joinery connectors that allow two single twin units to be locked together securely as a seamless King-size bed. Wall-mounted upholstered headboards feature sound-absorbing acoustic foam layers and integrated power socket cutouts.
Co-Living Spaces & Student Accommodation
Requirement: Maximized storage per footprint, scratch resistance, low maintenance.
Factory Solution: Lift-up twin bed frames featuring hydraulic gas-lift mechanisms revealing up to 0.6 cubic meters of dust-free under-bed storage. Frames are finished in high-pressure melamine laminate (HPL) edge-banded with 2mm impact-resistant ABS.
Multi-Family Real Estate & Build-to-Rent
Requirement: Aesthetic longevity, neutral contemporary appeal, fast installation.
Factory Solution: Architectural upholstered twin beds featuring removable, washable fabric covers in high-grade linen or microfiber. Knock-down construction allows easy elevator transport and rapid 15-minute two-person assembly per room.
Senior Living & Healthcare Residences
Requirement: Ergonomic support, rounded corners, anti-microbial surfaces.
Factory Solution: Soft-upholstered perimeter frames with radius-curved edges to minimize blunt force trauma. Water-repellent eco-leathers treated with anti-bacterial agents, combined with high-density ergonomic mattresses for optimal lumbar spinal alignment.
5-Stage B2B Customization Architecture
From preliminary architectural CAD interpretation to white-glove container consolidation, our structured project process guarantees zero discrepancy between design intent and delivered products.
Design & Specification Review
Client provides floor plans, architectural renderings, or material specs. Engineering team analyzes structural feasibility and proposes value-engineered material substitutes to meet target cost metrics.
3D Modeling & Prototyping
Precision CAD shop drawings and 3D digital mockups are generated. A physical pre-production sample is constructed within 7 to 10 days for structural testing, comfort calibration, and finish verification.
Compliance Certification
Upholstery fabrics, foams, and wood structures are submitted for required regional lab certifications (SGS, TÜV, Intertek) covering fire safety, formaldehyde emissions, and structural durability.
Automated Mass Production
Order schedules execute through ERP-managed CNC production lines. Dedicated QC managers conduct raw material checks, in-line frame audits, upholstery stitching inspections, and final pre-pack evaluations.
Export Crating & Container Loading
Items receive multi-layer protective packaging (EPE foam, corner guards, 5-ply corrugated cartons, wooden crates for fragile elements) and are loaded using space-optimization algorithms to maximize freight efficiency.
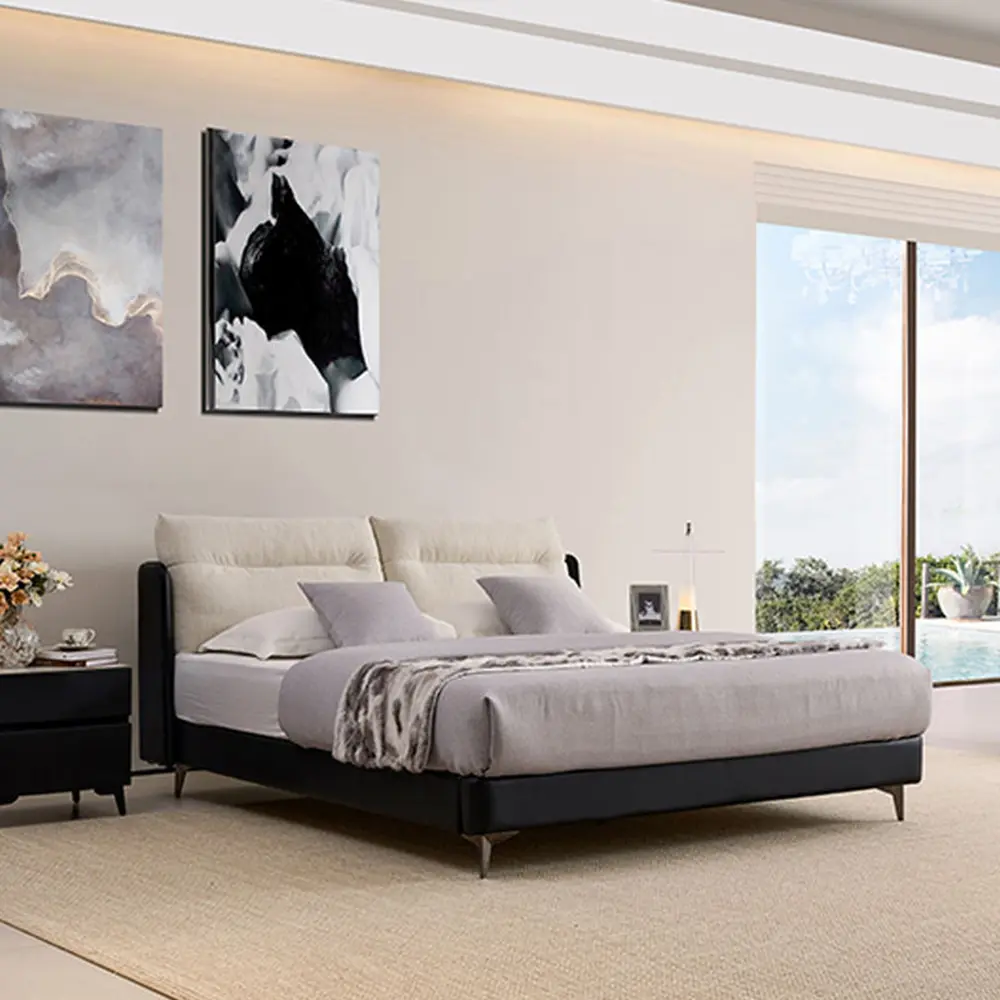
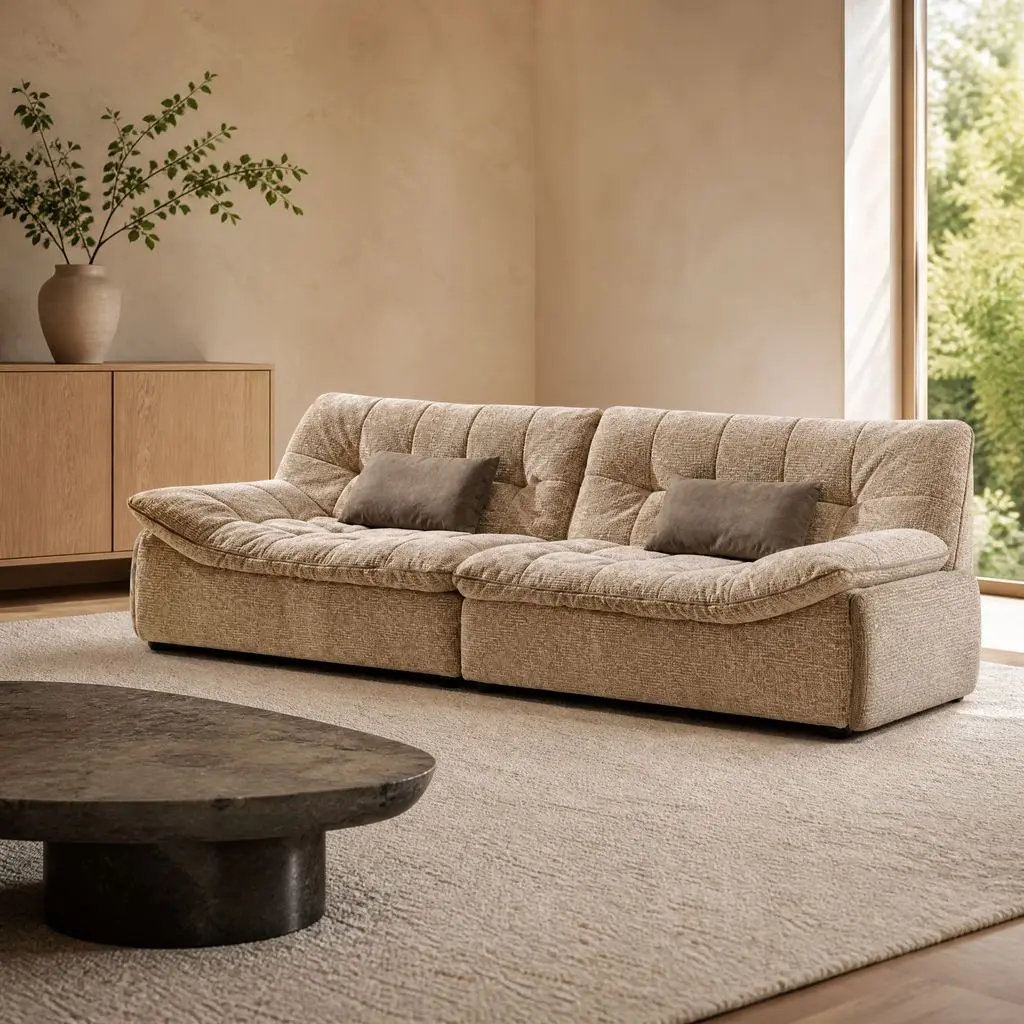
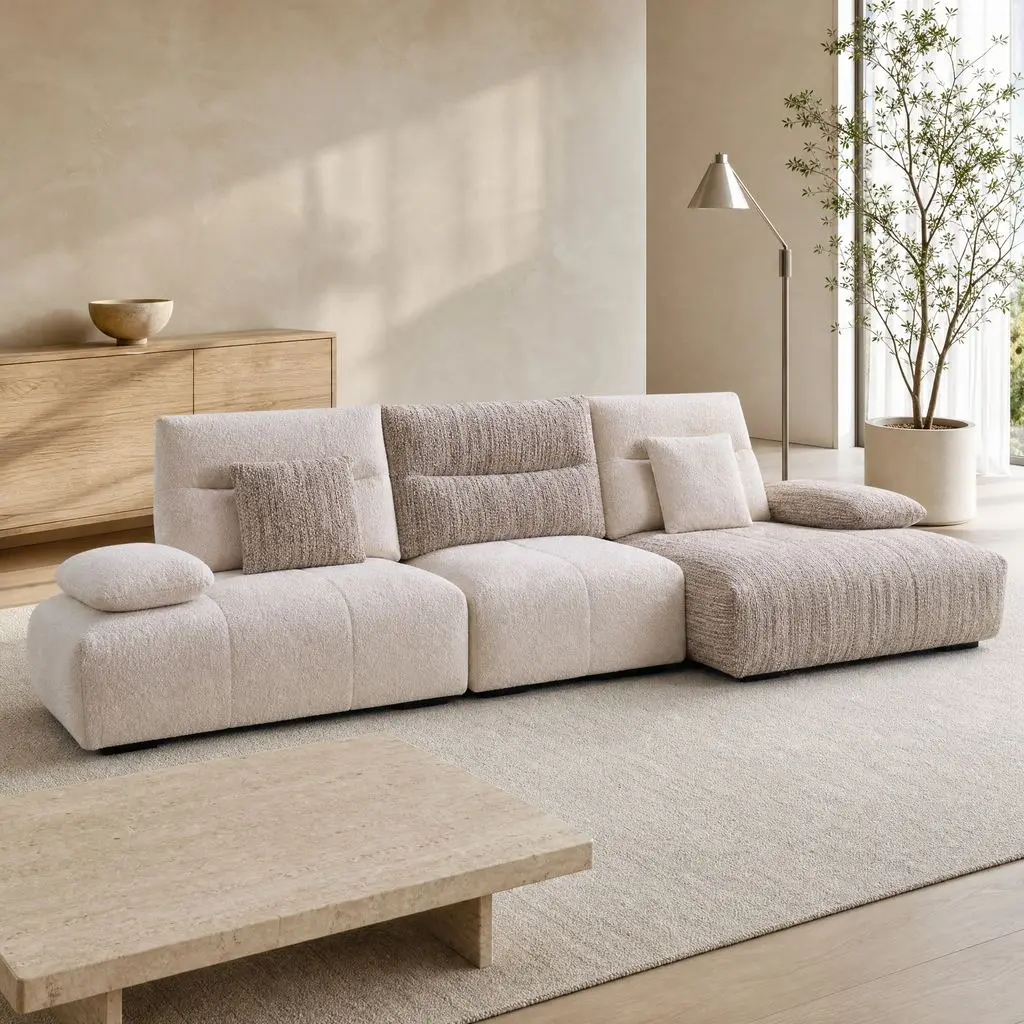
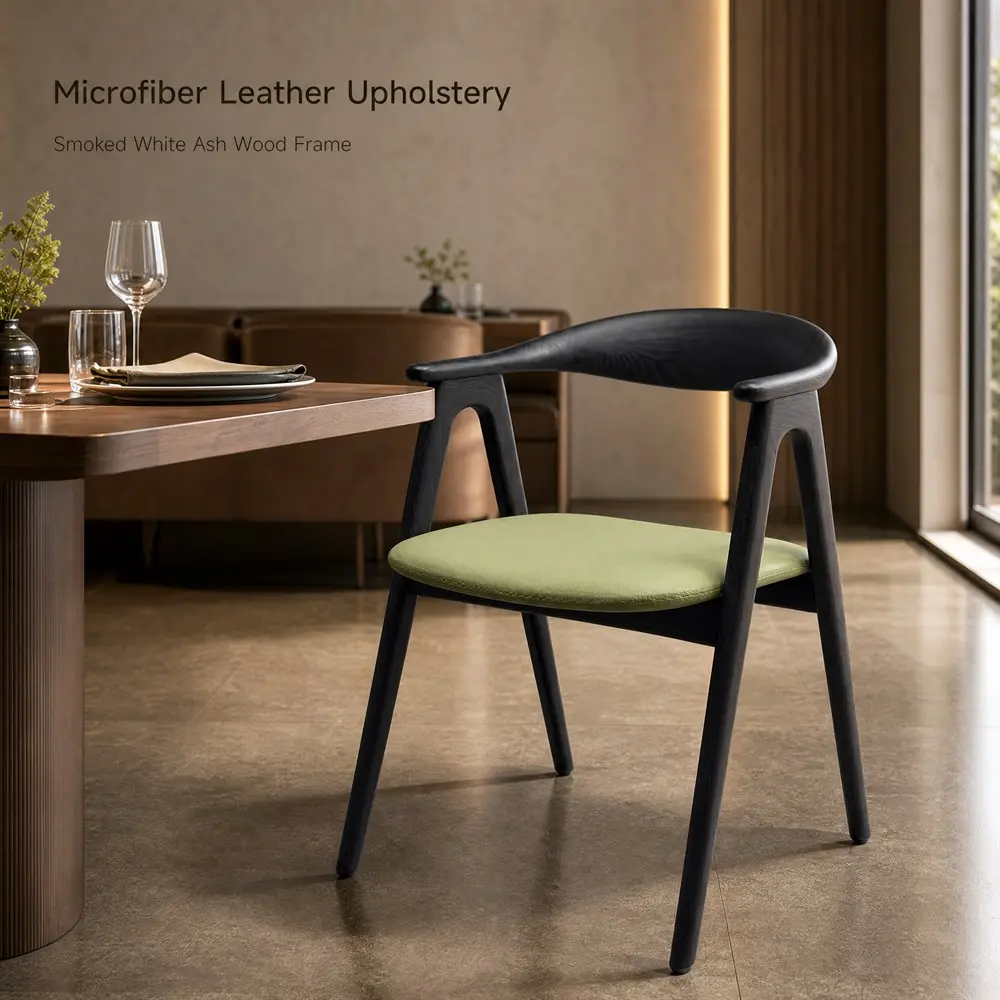
Expanded Bedroom, Dining & Lounge Collections
Integrated furniture solutions designed to harmonize aesthetic profiles across master suites, living rooms, and hospitality dining environments.
Industry FAQ: Strategic Procurement & Factory Sourcing
Addressing technical, logistical, and compliance questions frequently raised by global furniture buyers and contract project managers.