Featured Integrated Products (Top Selection)
Explore our flagship series engineered for commercial resilience, residential luxury, and global compliance. Each product represents rigorous material selection and Industry 4.0 production capabilities.
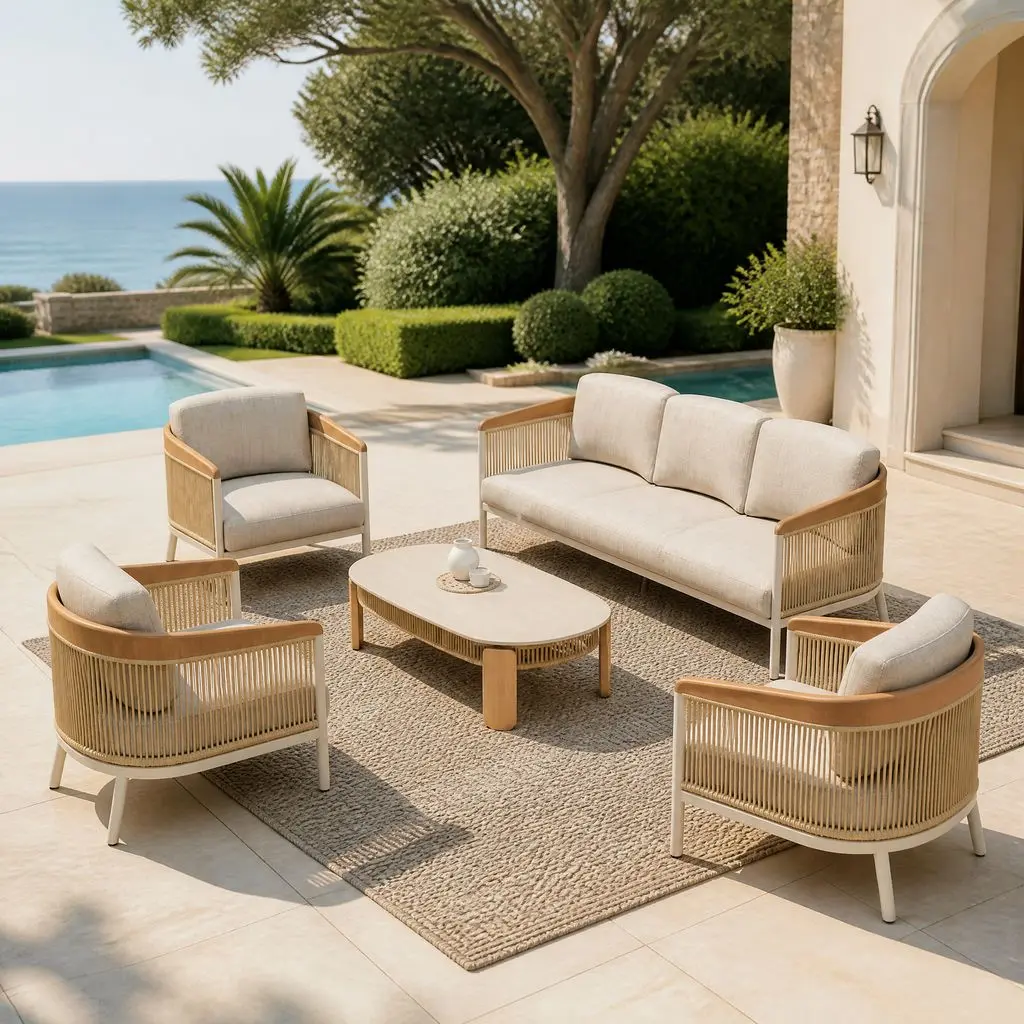
Wholesale QYM XD-6006 Modern Outdoor Sofa Set with Aluminum Frame, Teak Armrests, Woven Rope and Waterproof Cushions Manufacturer, Factories
View Specs
Latest design QYM C181 Leather Upholstered Bed Clean leather comfort for modern everyday bedrooms Factories, Wholesaler
View Specs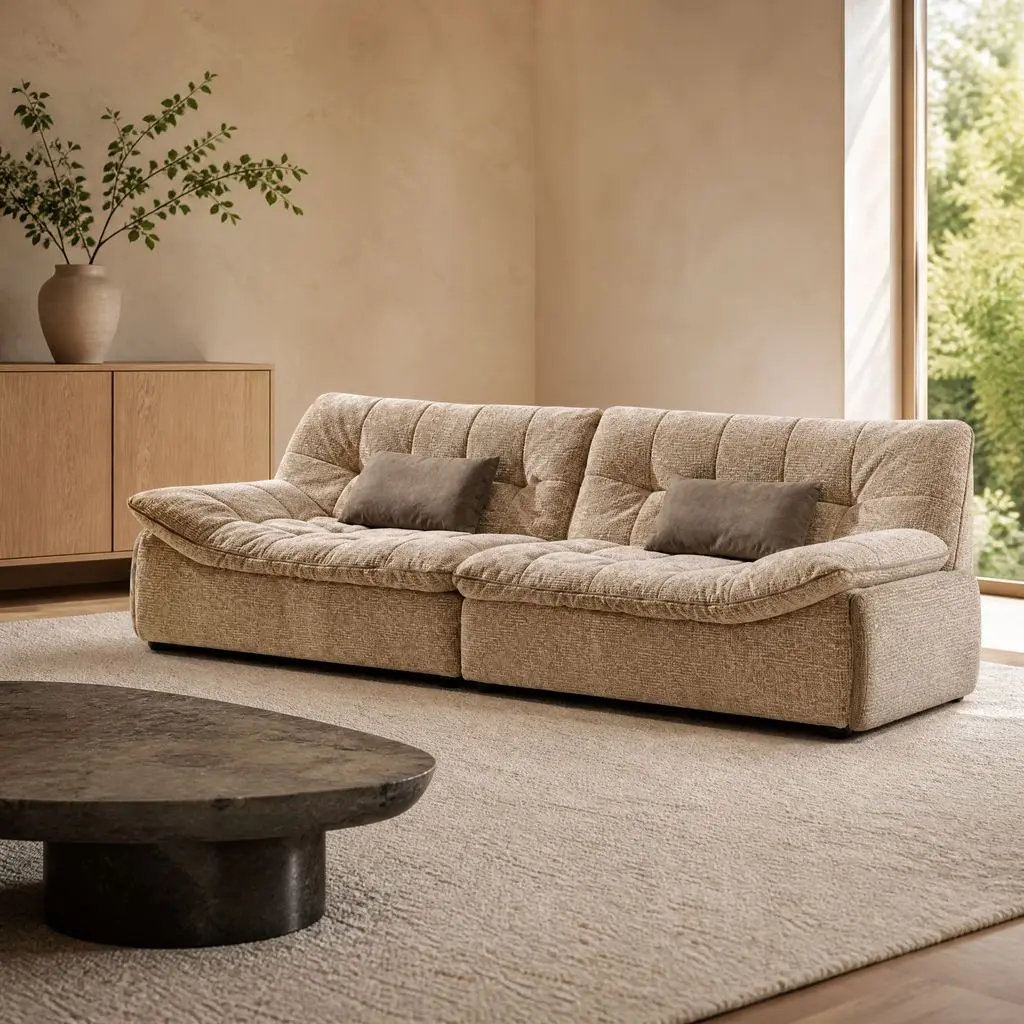
Wholesale QYM M1083 Modern Chenille Sectional Sofa with Latex Cushions, Imported Larch Frame, Solid Wood Legs and Washable Covers Supplier, Suppliers
View Specs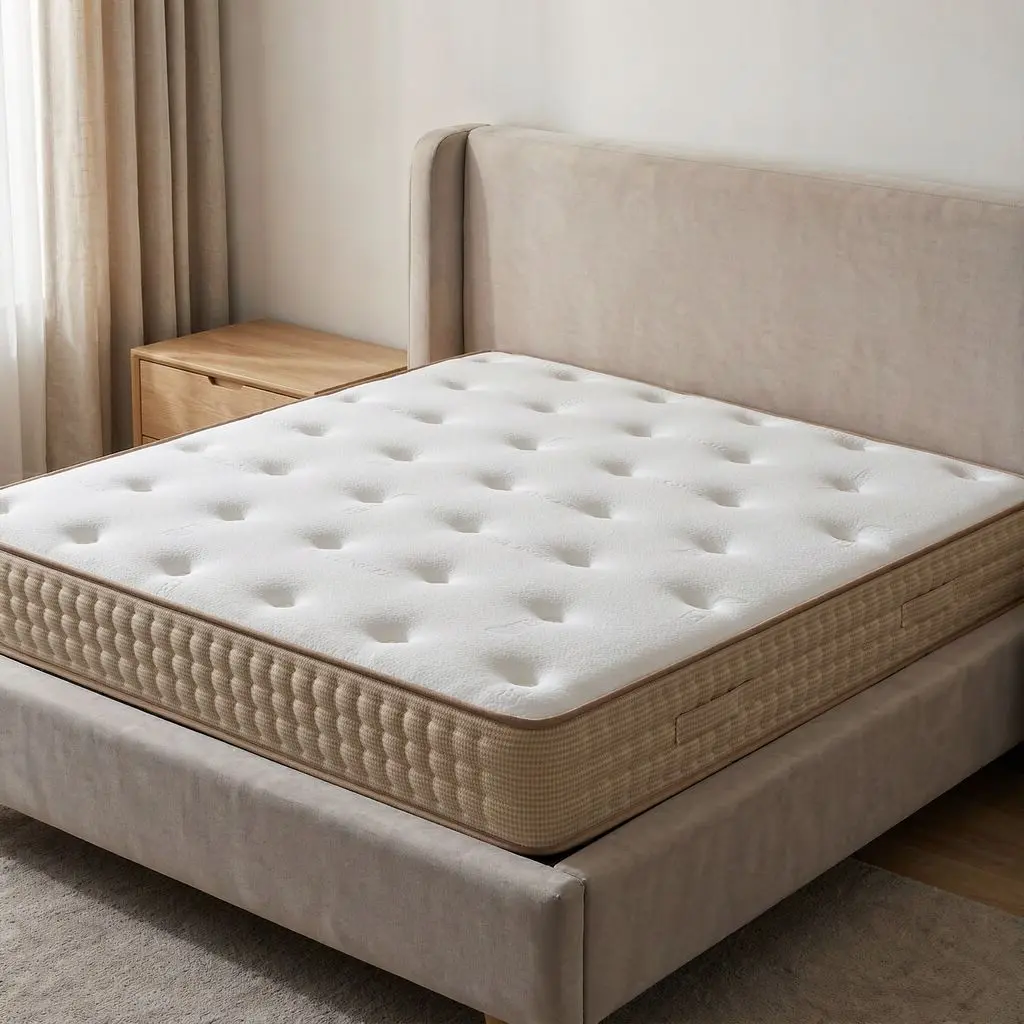
Latest design QYM SM-01 Handmade Mattress with Silent Pocket Springs, Memory Foam, Comfort Cotton and Premium Tencel Fabric Manufacturers, Factories
View Specs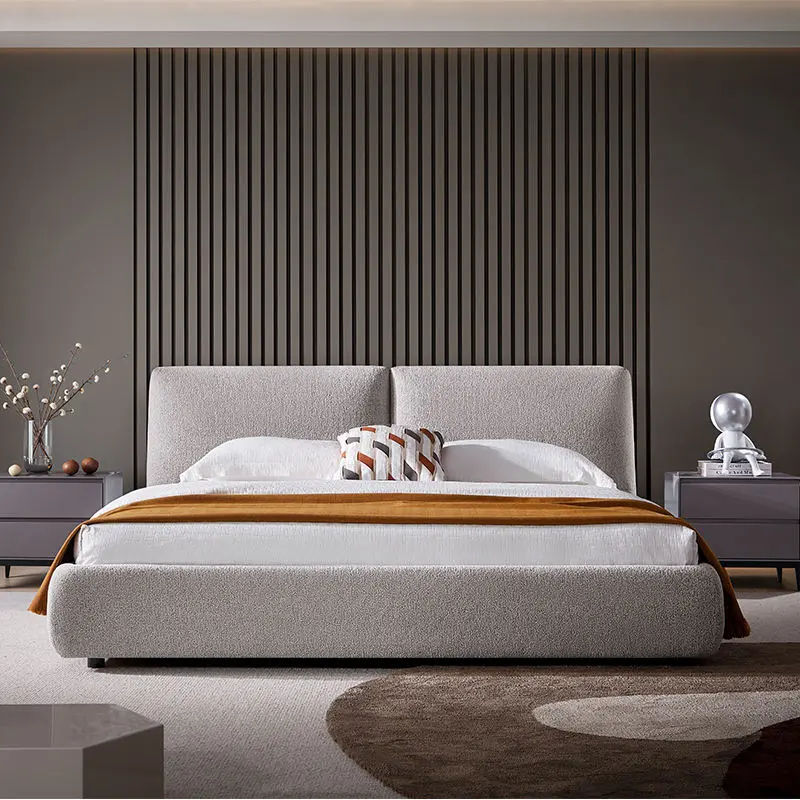
Wholesale QYM C179 New Design Modern Comfortable King Size Soft Bed with Integrated Storage & Quiet Steel-Wood Structure Manufacturers, Suppliers
View Specs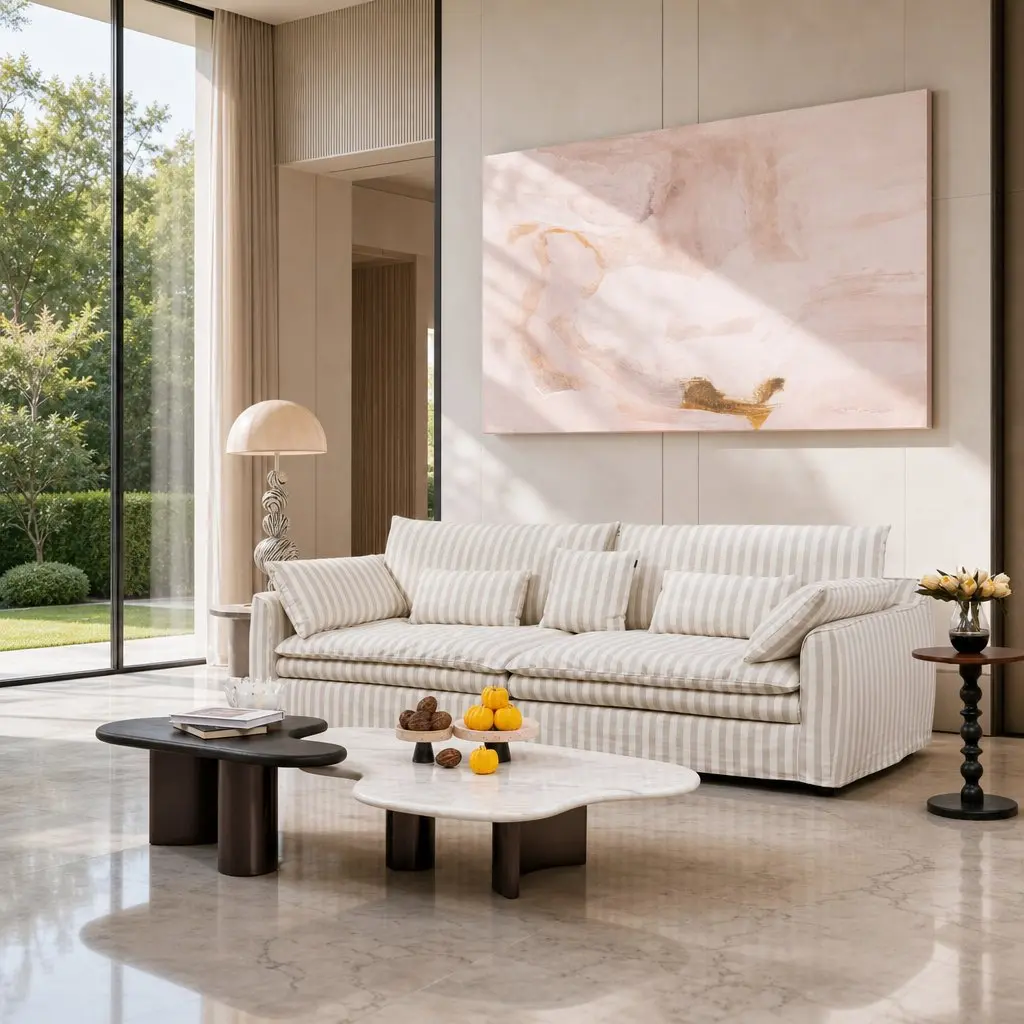
China QYM M1060 Modern Striped Linen Sofa with Imported Larch Wood Frame & Premium Natural Latex Down Silk Floss Filling - Fully Removable and Washable Luxury Sectional Couch for Living Room Supplier, Suppliers
View Specs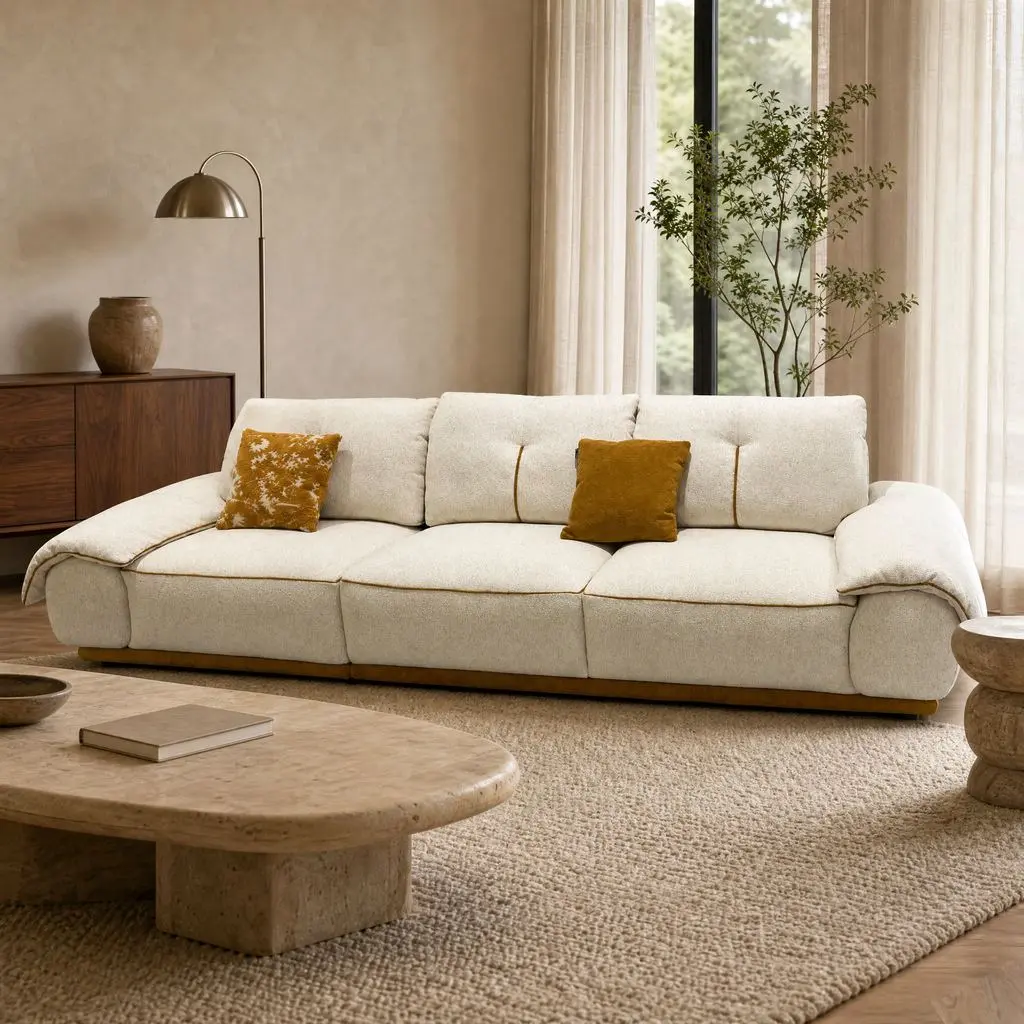
Wholesale QYM M1093 Modern Sectional Sofa with Mohair Plush Fabric, Larch Wood Frame, Solid Wood Legs, High-Density Foam and Washable Covers Suppliers, Factory
View Specs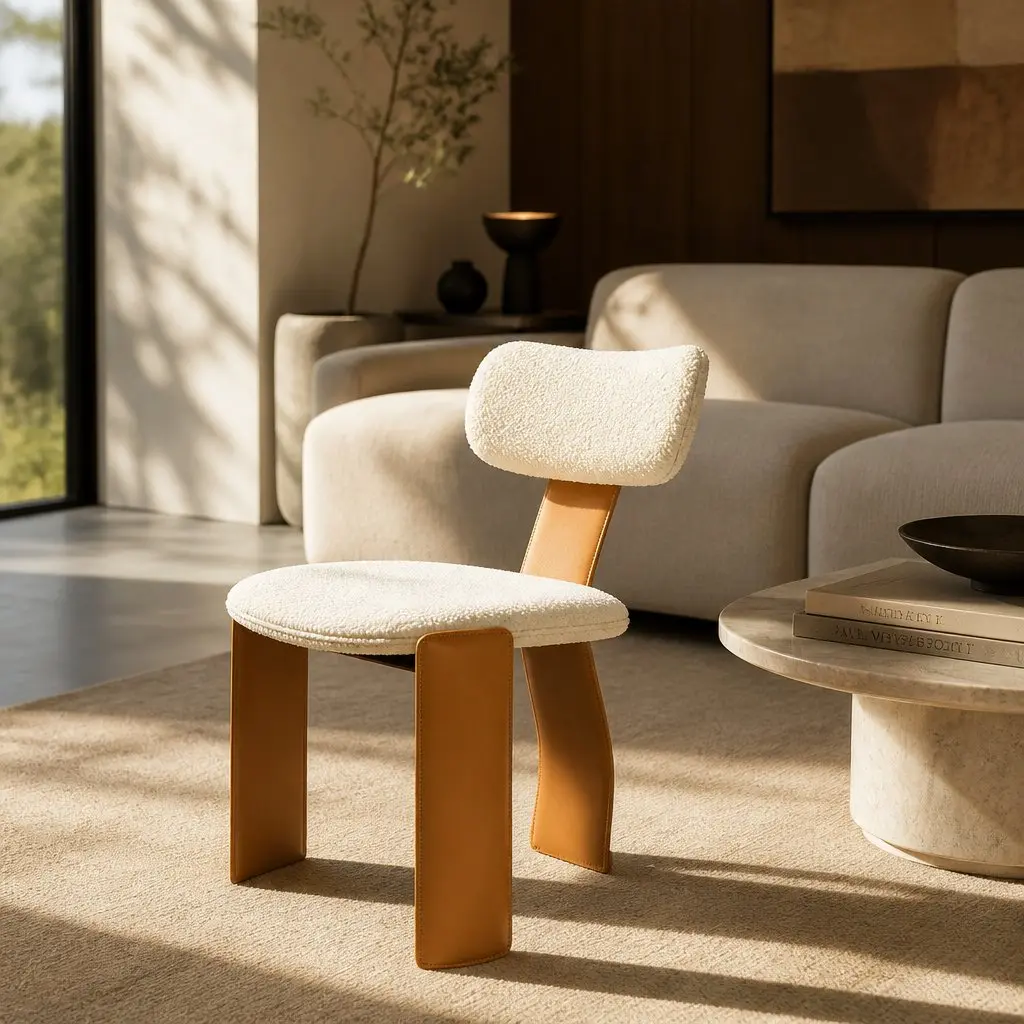
China White Bouclé Dining Chair, Italian Minimalist Accent Chair with Solid Wood & Stainless Steel Frame Suppliers, Factory
View Specs1. Executive Overview: Structural Evolution of the Marble Top Dining Table Sector
In the contemporary architectural and high-end furniture domain, the Marble Top Dining Table has transitioned from a purely decorative luxury statement into a highly engineered structural system. Modern B2B buyers—including enterprise furniture wholesalers, commercial interior design consultancies, and hospitality procurement executives—no longer evaluate marble dining tables solely on superficial veining patterns or slab aesthetic appeal. Instead, purchasing decisions are dictated by material density, flexural strength under variable loading, chemical stain resistance, structural thermal stability, and long-term maintenance overhead.
The global market demand for marble top dining tables has witnessed a significant structural shift. While natural organic stone (such as Italian Carrara, Arabescato, Calacatta Gold, and Greek Volakas) remains the gold standard for luxury residential developments and VIP hospitality suites, the advent of ultra-compact engineered stone—specifically Sintered Stone Slabs and high-density quartz composites—has revolutionized commercial food and beverage (F&B) environments. These engineered alternatives emulate natural marble veining while providing zero porosity, Mohs 6–7 scratch resistance, and immunity to acidic staining.
| Material Parameter | Natural Organic Marble Slab | Sintered Stone Composite Top | Engineered Quartz Stone |
|---|---|---|---|
| Mohs Hardness Scale | Mohs 3.0 – 4.0 (Requires protective sealant) | Mohs 6.0 – 7.0 (Highly scratch-resistant) | Mohs 6.5 – 7.0 (High scratch resistance) |
| Water Absorption Rate | 0.15% – 0.50% (Porous without impregnation) | < 0.02% (Ultra-impermeable, non-porous) | 0.03% – 0.05% (Stain resistant) |
| Flexural Strength (ASTM C880) | 10 – 18 MPa (Fragile on large spans) | 45 – 60 MPa (High flexural tolerance) | 30 – 45 MPa (Strong structural tolerance) |
| Thermal Shock Resistance | Moderate (Prone to thermal cracking) | Extreme (Direct thermal resistance up to 1200°C) | Moderate (Resin content degrades >150°C) |
| Primary Target Application | Executive Villas, Luxury Suites, Penthouse Dining | High-Traffic Restaurants, Commercial Hotels, Multi-Family | Commercial Dining, Office Conference Tables |
As a primary China-based manufacturer and global wholesaler, our production facility in Longjiang Town, Shunde District (Foshan), integrates advanced stone processing technology with structural sub-frame engineering. By pairing thin stone slabs with aircraft-grade aluminum honeycomb backing matrices and carbon-steel sub-structures, we eliminate the structural weight penalties historically associated with solid stone tables while multiplying impact resistance fourfold.
2. Technical Roadmap & Future Outlook in Marble Surface Engineering
To maintain a definitive edge in the competitive landscape of global furniture manufacturing, our R&D roadmap focuses on resolving the inherent physical limitations of natural marble through deep material science innovations. The future of marble top dining table manufacturing rests on four critical technology pillars:
Sub-Phase 1: Nano-Hydrophobic Sealing & Polymer Resin Impregnation
Natural marble consists primarily of calcium carbonate ($CaCO_3$), making it vulnerable to acidic corrosion from wine, lemon juice, and commercial clearing agents. Our engineering labs are pioneering vacuum-assisted epoxy resin impregnation combined with a fluoropolymer nano-sealant coating. This multi-stage treatment penetrates down to 3mm beneath the polished surface, creating an invisible hydrophobic barrier that achieves zero chemical etching while preserving natural stone touch and depth.
Sub-Phase 2: Lightweight Carbon Fiber & Aluminum Honeycomb Core Matting
Transportation and structural load limits are major cost drivers in international bulk shipments. Our future-focused manufacturing pipeline pairs 6mm ultra-thin natural marble or sintered stone surfaces with an 18mm high-density aluminum honeycomb lattice structure. Bound with structural polyurethane adhesives under 20-ton hydraulic compression, these composite slabs reduce overall table weight by 60% while increasing cantilever load capacity up to 350 kg.
Sub-Phase 3: Smart Surface Integration & Invisible Thermal Zones
As smart dining environments become standard in boutique hotels and executive residence projects, our engineering roadmap integrates invisible induction warming coils and Qi-certified wireless power transmission sub-layers directly beneath the marble veneer. Thermal diffusion management layers prevent micro-fracturing of natural marble veins, allowing the stone tabletop to maintain safe surface temperatures while keeping food warm.
Sub-Phase 4: Low-Carbon Stone Circular Sourcing & Zero-Waste CNC Milling
Aligning with global ESG policies and European Union carbon border adjustment mechanisms (CBAM), our production facilities utilize closed-loop water filtration systems during 5-axis CNC waterjet cutting. Off-cut stone matrices are reclaimed and transformed into terrazzo or engineered composite bases, ensuring a 94%+ material utilization efficiency rate across our manufacturing line.
3. Macro-Industry Solutions & Architectural Space Integration
Different market sectors demand highly specialized structural specifications. Our manufacturing architecture provides tailored end-to-end solutions across four major global B2B sectors:
Luxury Hospitality & Resorts
Designed for 5-star hotels, executive dining halls, and casino resorts. Features custom slab book-matching, stain-proof nano-sealers, and heavy-duty weighted metal sub-frames capable of withstanding constant commercial cleaning cycles and intensive daily use.
Multi-Family Residential Developments
Optimized for property developers and turnkey apartment contractors requiring standardized dimensions (e.g., 1600mm, 1800mm, 2000mm length), high impact resistance, modular knockdown (KD) bases, and compact palletizing for rapid installation.
Wholesale Importers & Distributors
Engineered for commercial furniture brands and regional wholesalers. We offer private labeling, customized OEM/ODM packaging, optimized container space packing (up to 220 dining tables per 40HQ container), and complete digital marketing assets.
4. China Factory 4.0: Supply Chain Resilience & Manufacturing Precision
Located in Shunde District, Foshan City—the recognized epicenter of global furniture production—our manufacturing ecosystem integrates automated raw material sourcing, robotic stone cutting, and multi-stage structural quality control. This concentration of raw material suppliers, precision tool makers, and specialized export logistics hubs provides unmatched cost efficiency and agility.
5-Axis CNC Waterjet & Beveling Tech
Our factory utilizes computer-guided 5-axis CNC waterjet cutting tools operating under ultra-high pressure (410 MPa). This enables seamless 45-degree chamfering, bullnose edge execution, and intricate custom organic table shapes with tolerances under $\pm 0.5\text{mm}$. Micro-fractures along edge bevels are completely eliminated through multi-stage diamond polishing wheels.
Rigorous QA & Slab Structural Testing
Every batch of natural marble and sintered stone slabs undergoes rigorous non-destructive ultrasonic testing to detect internal fissures prior to cutting. Assembled table bases undergo dynamic 300 kg static load testing and 24-hour salt-spray corrosion testing for all stainless steel, PVD titanium, and powder-coated metal sub-frames.
5. Global Enterprise Procurement Needs & Customization Framework
Procurement for enterprise-scale commercial and wholesale projects requires flexibility in material customization, dimensions, structural framing, and specialized protective export packaging. Our engineering division operates a fully modular manufacturing workflow:
1. Slab Material & Pattern Matching
Select from premium Italian natural marbles, Brazilian quartzites, or ultra-durable sintered stone slabs. Options include symmetrical book-matching, continuous veining, polished high-gloss finishes, hone-matted tactile finishes, and leathered organic textures.
2. Base Structural Engineering
Base structures are custom engineered utilizing 304/316 stainless steel with vacuum PVD titanium coating, die-cast aluminum legs, solid imported larch wood internal cores, or carbon steel with electrostatic powder coating to match specific architectural hardware finishes.
3. Heavy-Duty Export Packaging
To safeguard brittle stone surfaces across ocean transit, tables are packaged in ISPM-15 compliant fumigated solid plywood crates. High-density EPE foam padding, corner guards, and vacuum-sealed plastic wrap guarantee zero transport loss.
6. Localized Support & International Compliance Guarantees
Navigating international trade standards requires meticulous compliance documentation and dependable post-sale logistics support. Foshan Qingyumai Technology Co., Ltd. provides full compliance backing for global destination ports:
Regulatory Standards & Certifications
Our products comply with European Union REACH chemical regulations, CE structural safety standards, and North American ASTM C170 (Compressive Strength) & ASTM C99 (Modulus of Rupture) stone testing protocols. Timber elements utilized in sub-frames are FSC certified and comply with US EPA TSCA Title VI / CARB Phase 2 formaldehyde emission limits.
End-to-End Logistics & DDP Services
Our dedicated international trade department coordinates FOB (Foshan/Shenzhen/Guangzhou), CIF, and DDP (Delivered Duty Paid) shipping options. Our post-sale team manages full container loading space optimization, custom clearance documentation, door-to-door delivery logistics, and provides detailed CAD assembly guidelines for installation teams.
7. Frequently Asked Questions (Technical & Procurement FAQ)
Direct insights for commercial procurement managers, importers, and project engineers evaluating bulk orders for marble top dining tables and integrated furniture packages.
Q1: What is the primary functional difference between natural marble and sintered stone table tops for bulk commercial orders?
Natural marble offers authentic, one-of-a-kind organic geological veining and prestige, making it ideal for high-end luxury residential and VIP suites. However, natural marble is porous and requires periodic sealant maintenance. Sintered stone is an engineered matrix produced under extreme temperature (1200°C+) and pressure (30,000+ tons). Sintered stone tops are zero-porous (<0.02% water absorption), highly scratch-resistant (Mohs 6–7), heat resistant, and maintenance-free, making them the preferred choice for high-traffic commercial food service and multi-family projects.
Q2: How does your factory prevent marble tops from cracking during ocean freight transit?
We utilize a three-layer protection protocol: First, stone tops are reinforced on the underside with a fiberglass mesh or aluminum honeycomb composite matrix. Second, table edges and corners are fitted with custom EVA protective rubber caps. Third, slabs are packed flat or at a precise 80-degree incline inside fully enclosed, ISPM-15 compliant fumigated plywood crates reinforced with internal steel banding to absorb shock during container transportation.
Q3: What are your Minimum Order Quantity (MOQ) and lead times for wholesale OEM/ODM projects?
Our standard MOQ for wholesale dining tables is 5 to 10 units per design, with mixed-container consolidation allowed across our living room, bedroom, and outdoor collections. Standard production lead times range between 20 to 30 days depending on slab availability and customization complexity. Expedited sampling is available in 7 to 10 days.
Q4: Can we mix dining tables, upholstered chairs, beds, and sofas into a single container order?
Yes. Qingyumai specializes in whole-house and contract project consolidation. You can combine up to 19 distinct furniture categories under a single purchase order, single quality inspection standard, and unified shipping schedule, significantly lowering ocean freight costs per unit.
Q5: How do you handle custom dimensions, base finishes, and book-matched slab requirements?
Our internal CAD engineering team translates architect drawings or client specs into 3D production models within 24 hours. Slabs are digitised via high-resolution optical scanners, allowing clients to preview exact vein placement and book-matching patterns prior to 5-axis CNC waterjet cutting.
Complete Whole-House & Commercial Collection (Bottom Selection)
Discover our extended line of upholstered beds, ergonomic mattresses, modular sectionals, and outdoor systems designed for seamless integration with our marble dining collections.
China QYM C166 Leather Upholstered Bed Manufacturer, Supplier
View Specs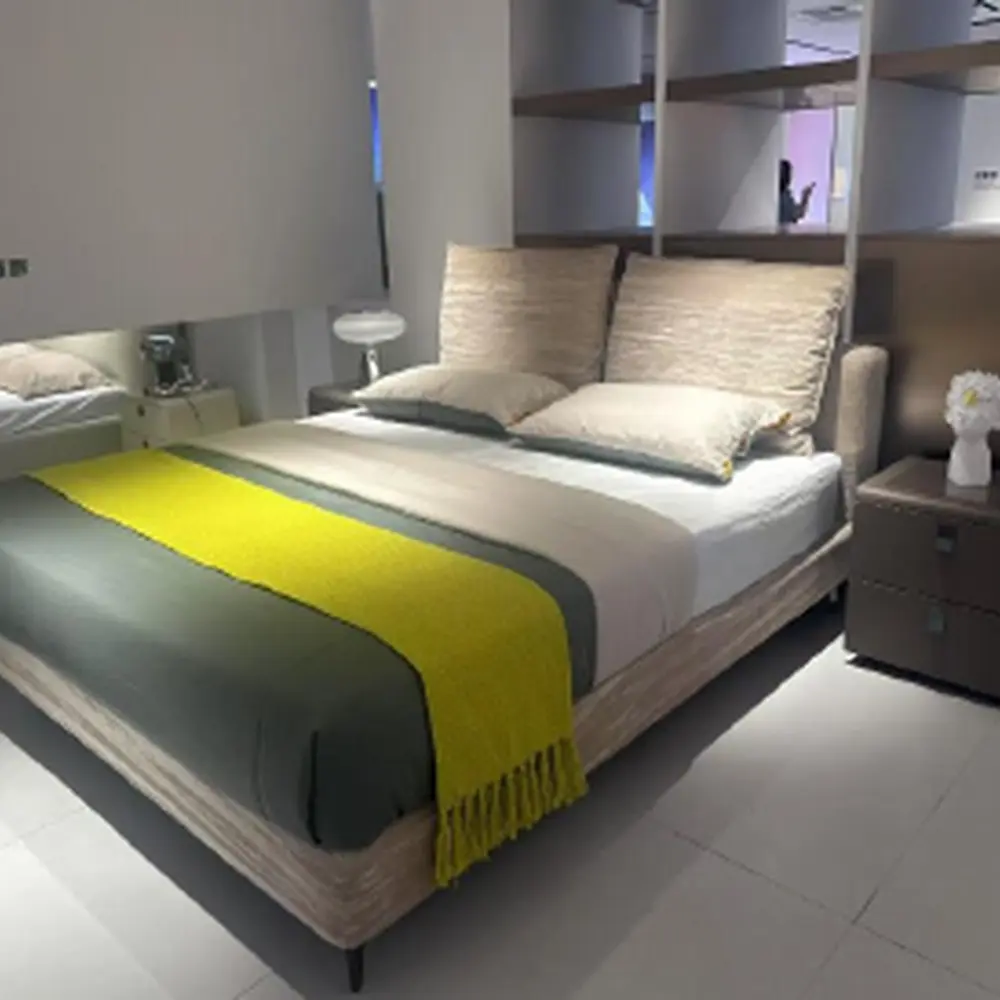
Latest design QYM C201 Chenille Upholstered Bed Soft chenille texture with a composed modern silhouette Suppliers, Wholesaler
View Specs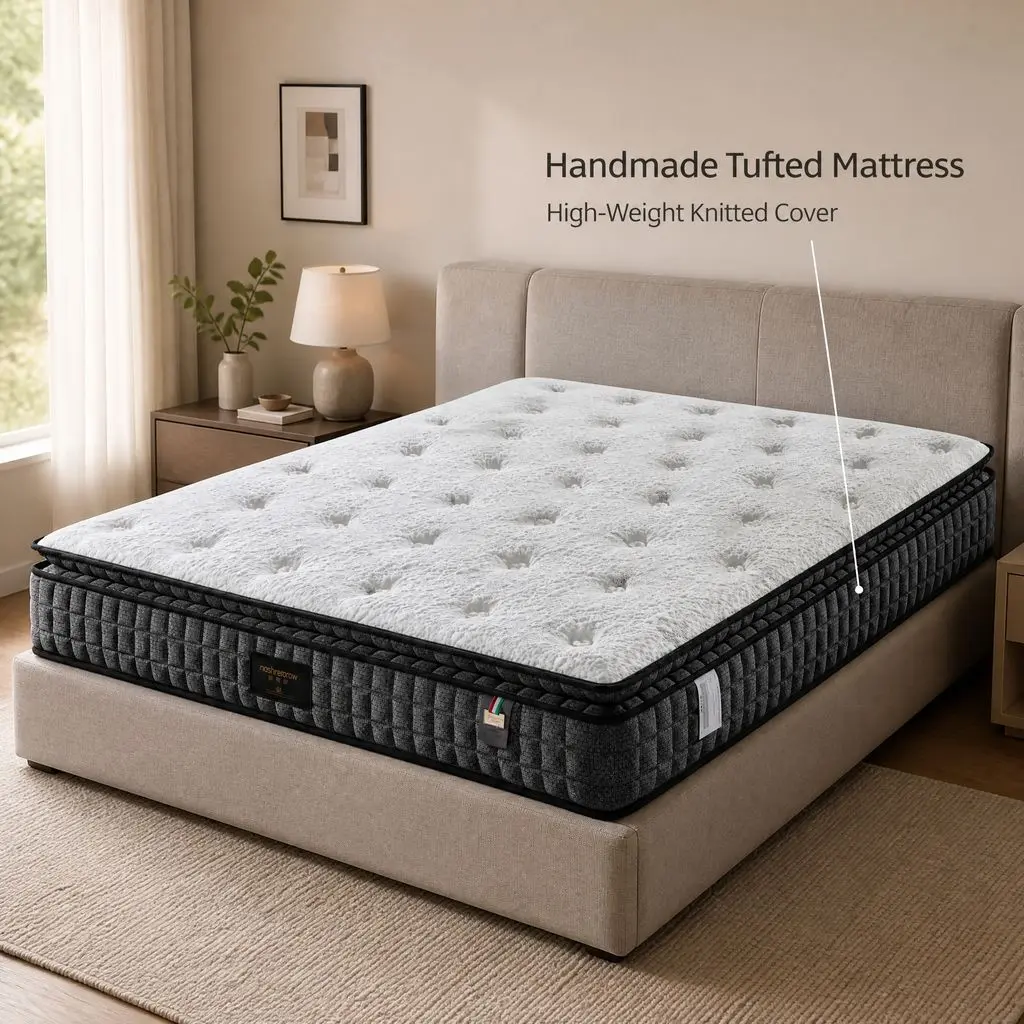
Wholesale QYM NYFX01 Handmade Mattress with Cool-Touch Pocket Springs, Cloud Memory Foam and High-GSM Knitted Fabric Manufacturers, Manufacturer
View Specs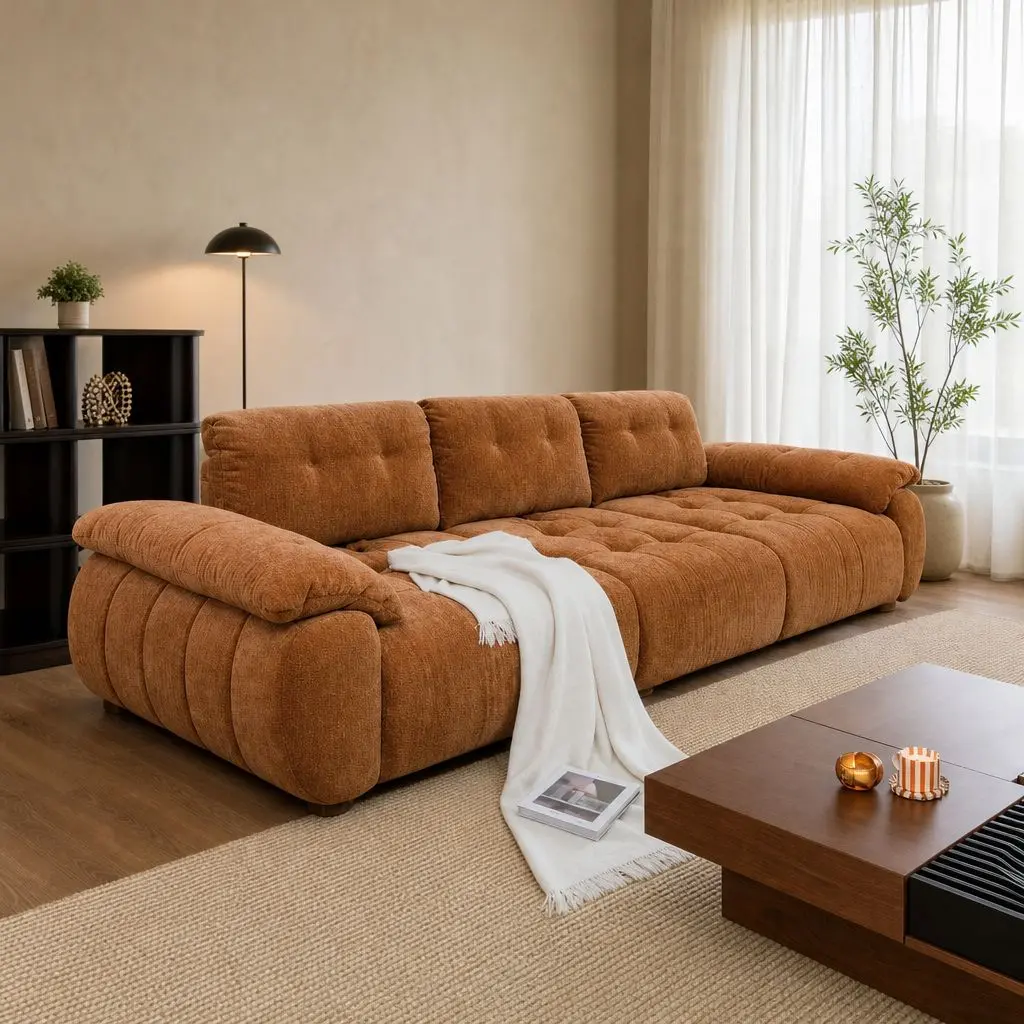
Latest design QYM B2212 Modern Functional Sectional Sofa with Two-Tone Linen, Larch Wood Frame, High-Density Foam and Washable Covers Suppliers, Wholesaler
View Specs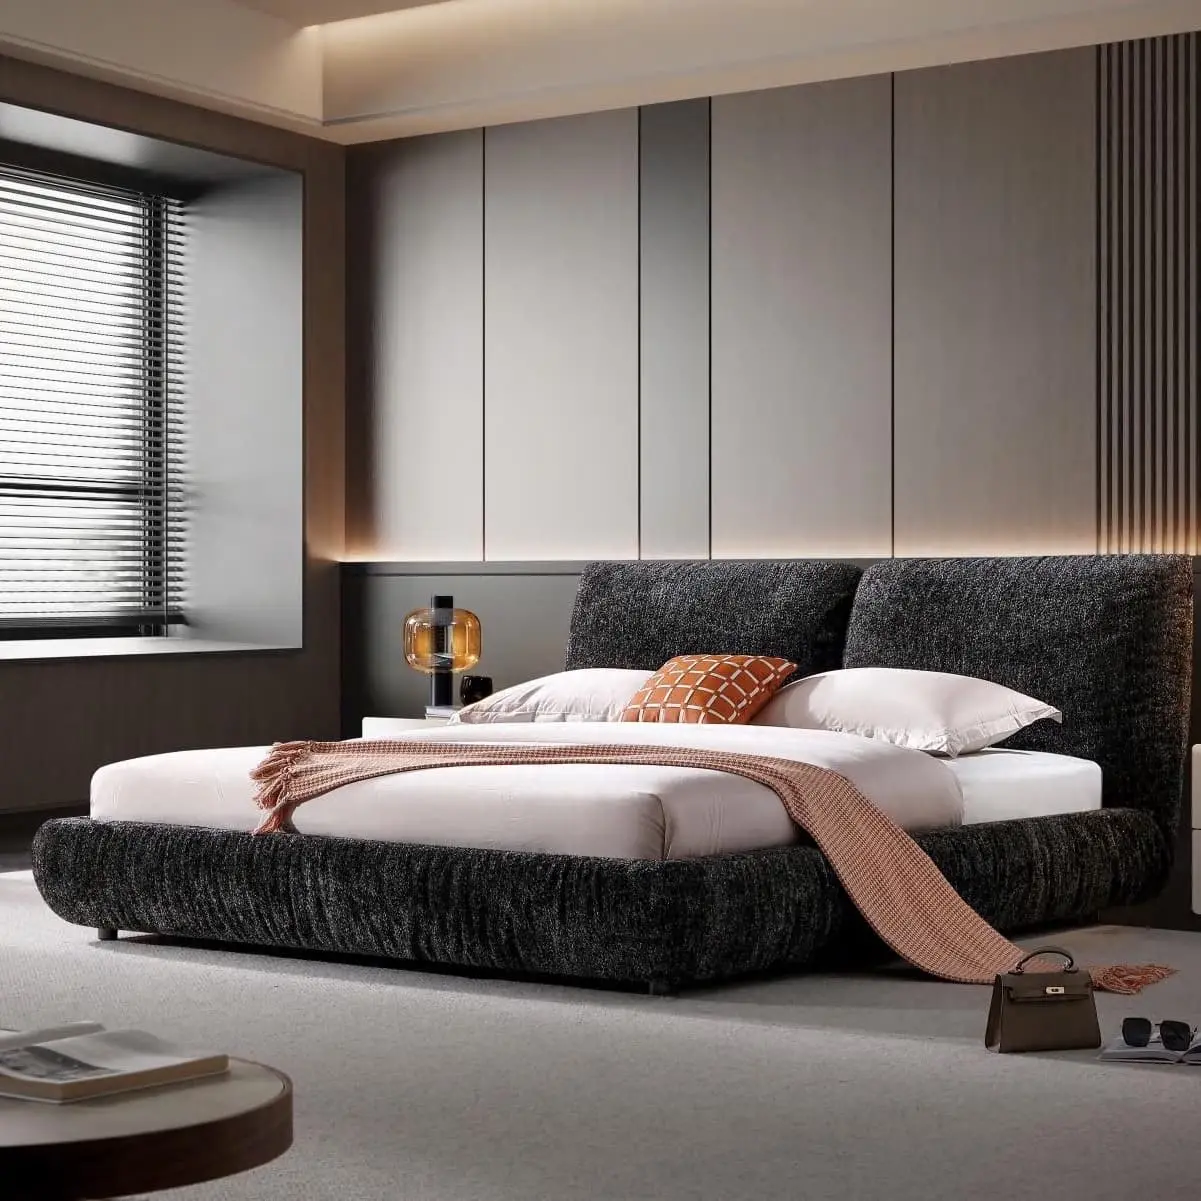
Wholesale C222 Fabric Upholstered Bed A generous low-profile bed with relaxed textile appeal Supplier, Factories
View Specs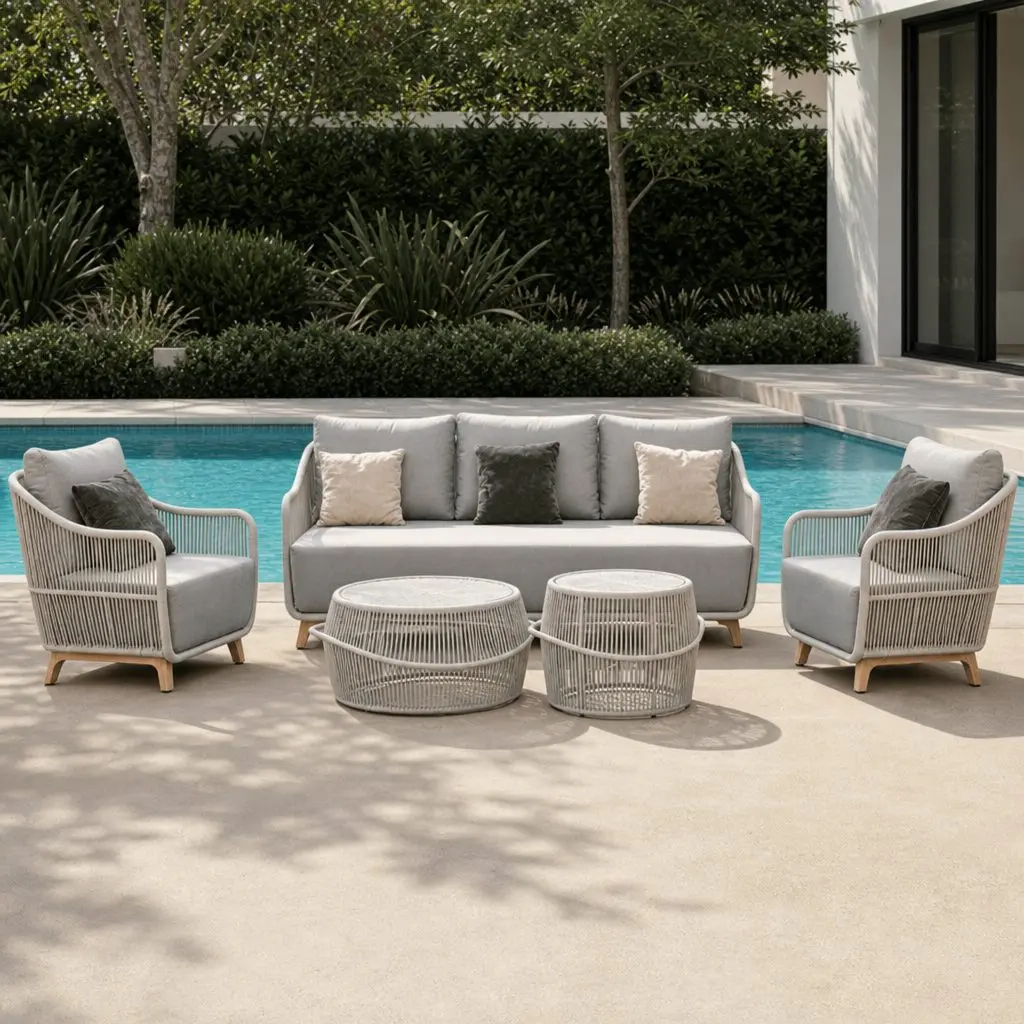
Wholesale QYM XD-6017 Armless Outdoor Sofa Set with Wood-Grain Aluminum Frame, Olefin Rope Weave and Teak Backrest Manufacturer, Suppliers
View Specs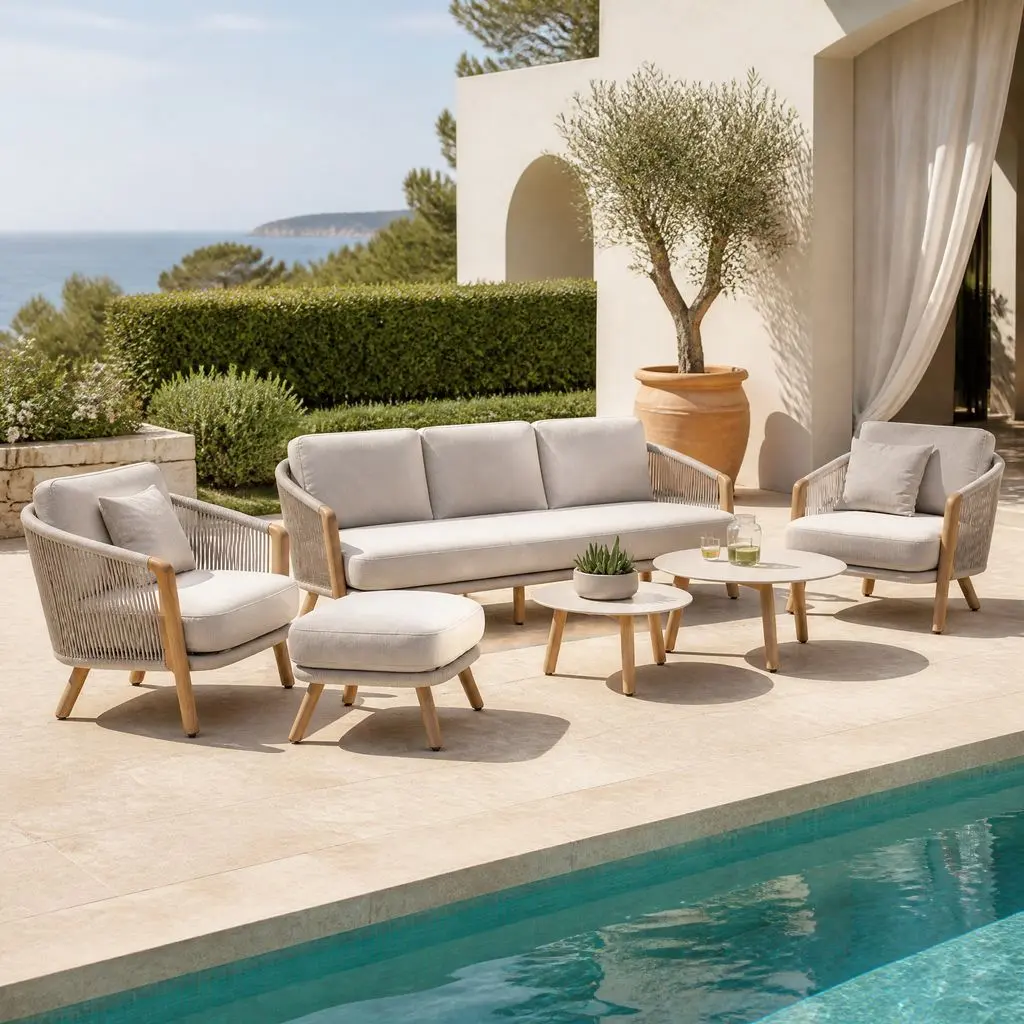
Latest design QYM XD-6001 Outdoor Rope Sofa Set with Wood-Grain Aluminum Frame, Waterproof Cushions and Teak Armrests Supplier, Factories
View Specs