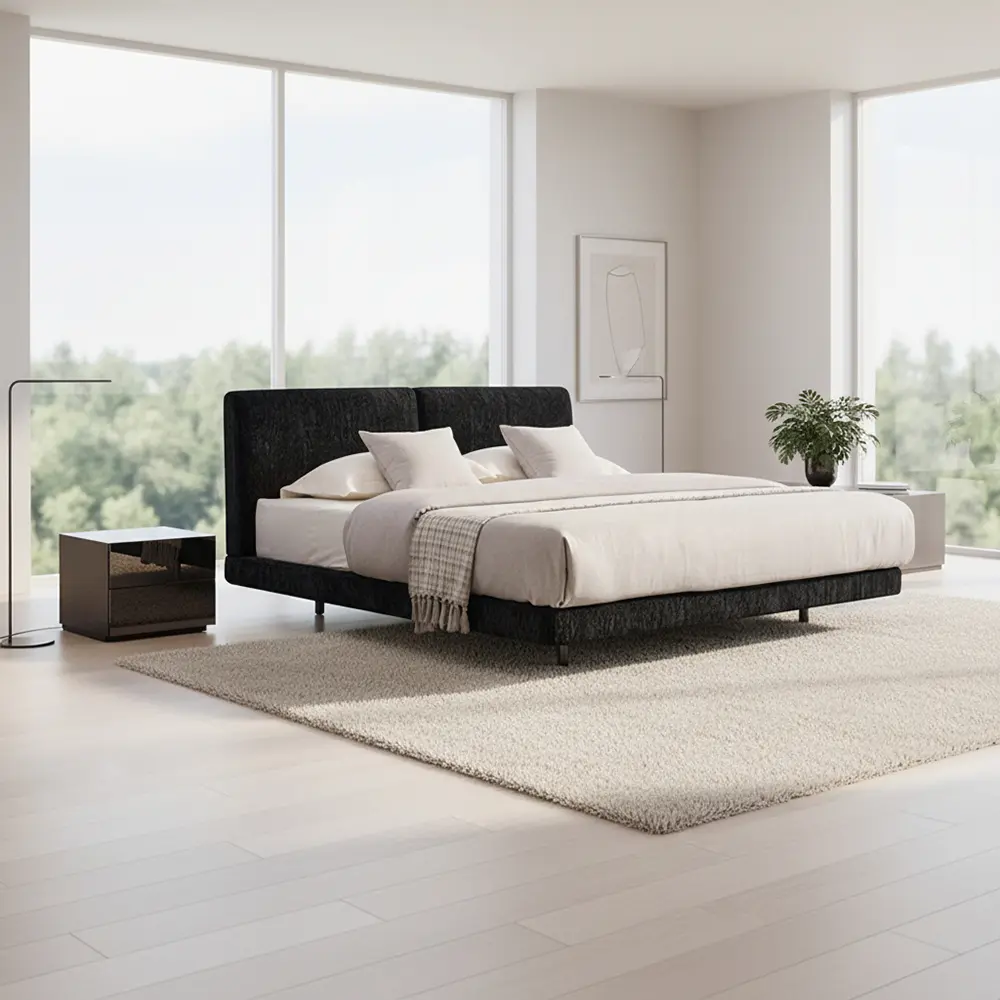
Featured OEM Export Collections (Part I)
Explore our export-grade furniture and mattress solutions engineered for high compression ratios and international transit safety.
Executive Overview: The Evolution of Compressed Mattress Manufacturing
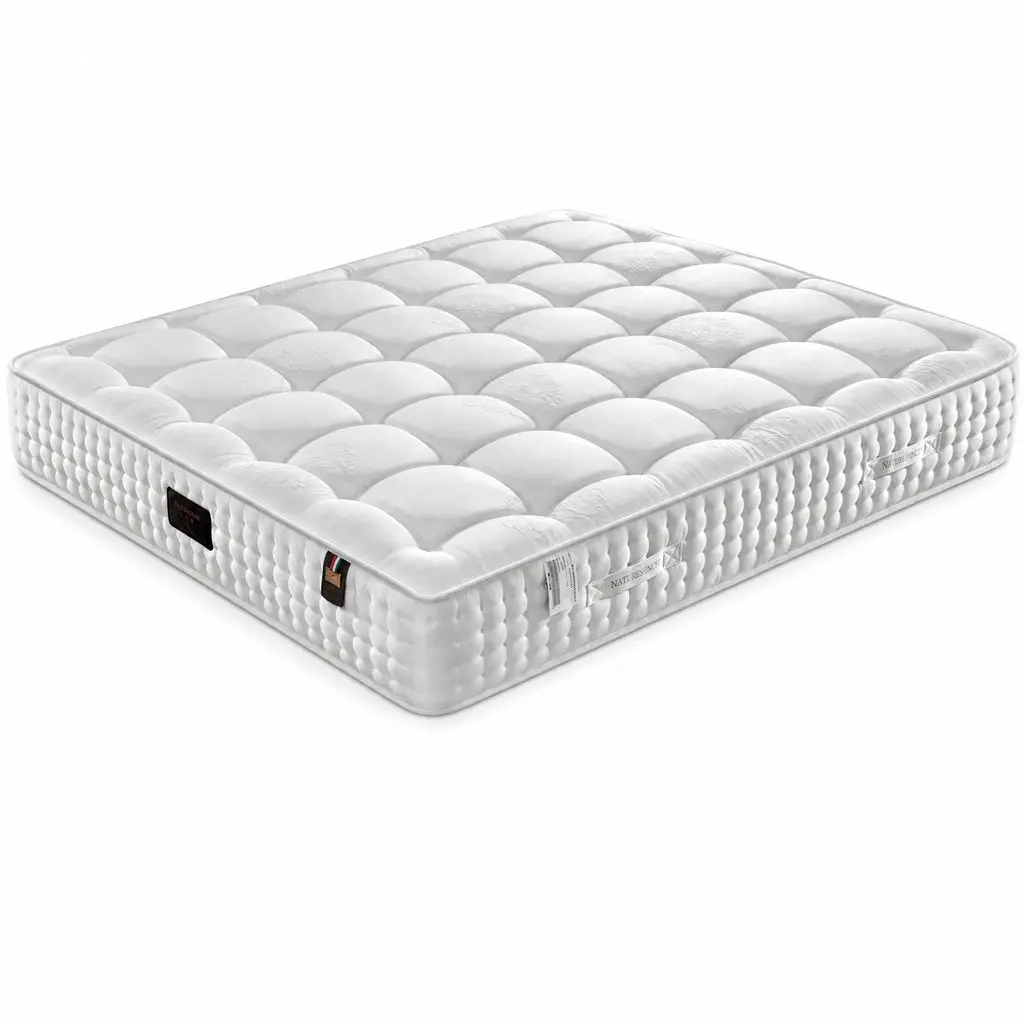
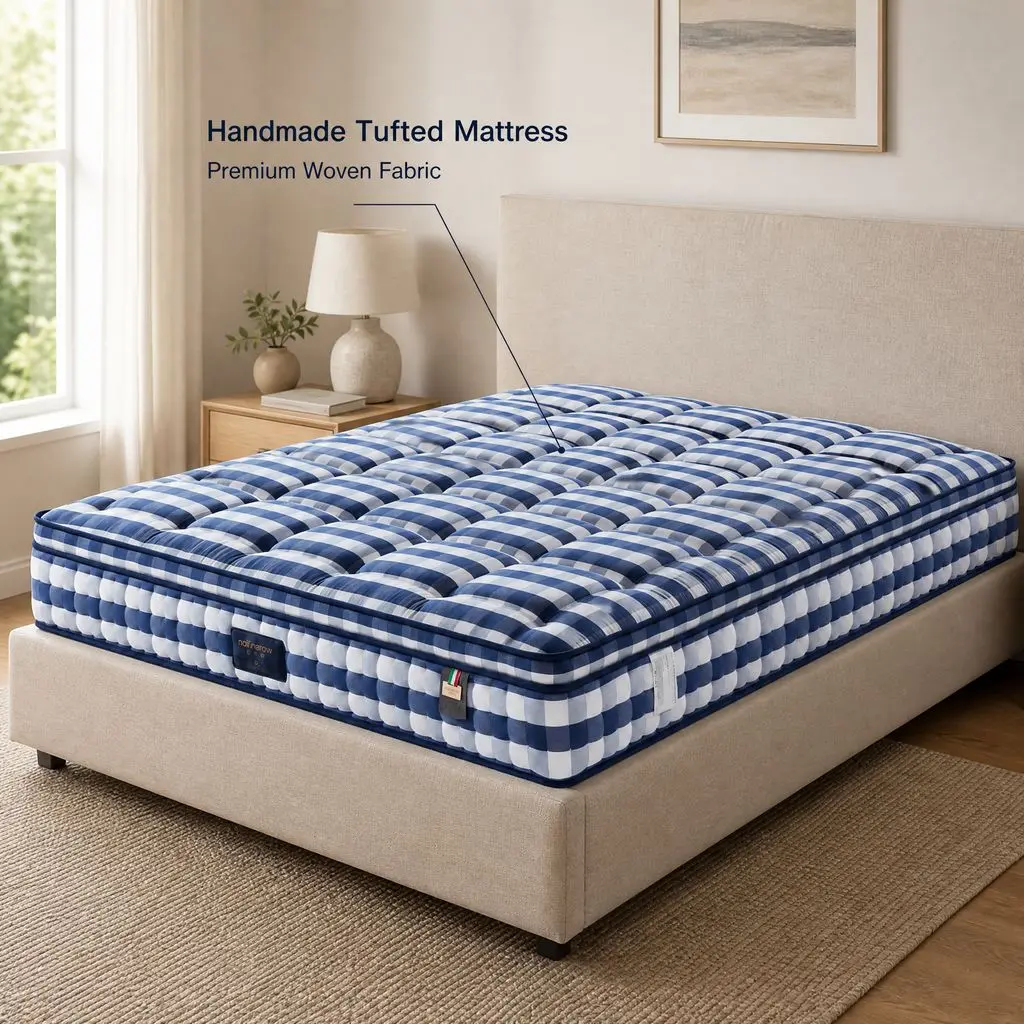
The global sleep technology industry has undergone a radical paradigm shift over the past decade. Driven by exploding e-commerce logistics costs, shifting consumer preferences toward bed-in-a-box delivery models, and high-density urban living, the demand for high-performance compressed mattresses has accelerated globally. As a leading enterprise among Wholesale Compressed Mattress Manufacturers & Wholesalers, engineering excellence is no longer measured solely by surface comfort, but by complex mechanical compression ratios, structural memory retention, and long-term spring resilience.
Historically, traditional innerspring mattresses required immense volumetric space during ocean transport, leading to exorbitant shipping costs per unit. The advent of automated roll-packing technology—combining multi-ton hydraulic pressure flat-packing with high-speed automated rolling—allows a full-size pocket spring mattress to be reduced to less than 25% of its original cubic volume. However, achieving this degree of compression without causing permanent foam cell collapse, wire deformation, or border wire destruction requires sophisticated metallurgy, advanced polyurethane formulation, and stringent process controls.
For B2B buyers, furniture importers, hospitality developers, and retail brand owners, partnering with a technologically advanced manufacturer in China's prime production cluster (Foshan Shunde) provides a distinct competitive edge. This whitepaper analyzes the engineering frameworks, materials science, logistics strategies, and regulatory frameworks required to successfully procure compressed mattresses at industrial scale.
Compressed Mattress Technical Roadmap & Future Outlook
The transition from basic foam roll-packing to advanced multi-layer hybrid compressed mattresses represents a significant technological leap. Manufacturers must resolve complex material dynamics: how do viscoelastic memory foams, natural Thai latex, non-woven pocket spring encasements, and high-tensile steel coils react under 40 tons of continuous hydraulic press force over months of international sea transit?
Coil Wire Metallurgy & Tempering
Our spring systems utilize 65Mn or 70# high-carbon steel wire subjected to electric secondary heat tempering. This prevents elastic fatigue, allowing 99.8% coil height recovery post-decompression even after 180 days in vacuum packaging.
Open-Cell Polyurethane Foams
Traditional closed-cell foams trap air and burst cell walls under extreme hydraulic compression. We utilize open-cell MDI-based polyurethanes engineered with high gel content that flex rather than fracture under multi-ton load stress.
Ultrasonic Non-Woven Pocket Seams
To prevent internal pocket spring row displacement during high-speed cylindrical rolling, pocket sleeves are welded using 28kHz ultrasonic heat seals, maintaining tensile bond strength above 85N per seam line.
Smart Sensor Integration
Next-gen compressed mattresses are now incorporating ultra-thin, flexible piezoelectric sensor arrays and conductive silver yarn knitted directly beneath the quilting layer, remaining functional post-roll compression.
Information Gain Insight: The Physics of "Compression Fatigue"
Many low-cost factories experience severe product returns due to "sagging edges" or "permanent body indentations" after compressed unboxing. The root cause is micro-fracturing of polyurethane cell struts when compressed beyond their ultimate yield point. By utilizing MDI (Methylene Diphenyl Diisocyanate) raw chemistry combined with natural vegetable polyols (castor oil derivative) and 7-zone localized density mapping, our factory eliminates cell collapse while increasing breathability and thermal dissipation.
Material Recovery Comparison Matrix
| Material Layer | Standard Density | Compression Resistance (6 Months) | Unboxing Recovery Time | Primary Industrial Benefit |
|---|---|---|---|---|
| 65Mn Heat-Treated Pocket Coils | 2.0mm - 2.3mm wire | > 99.5% Height Retention | Immediate (< 30 Seconds) | Independent motion isolation & structural spinal support |
| MDI Open-Cell Gel Memory Foam | 45 kg/m³ - 60 kg/m³ | > 98.2% Density Recovery | 12 to 24 Hours | Targeted pressure point relief & micro-climate control |
| Thai Natural Latex (Pin-Core) | 75 kg/m³ - 85 kg/m³ | > 99.0% Elastic Recovery | Immediate (< 2 Minutes) | Hypoallergenic, buoyant comfort layer with high airflow |
| High-Resilience Support Foam (HR) | 32 kg/m³ - 40 kg/m³ | > 97.5% Tensile Strength | 2 to 4 Hours | Base structural foundation preventing bottom-out feeling |
Macro Industry Solutions & Freight Optimization
In modern global trade, logistics is often the single largest variable influencing landed product cost. Standard uncompressed mattresses severely underutilize container cubic capacity, effectively forcing brand owners to pay thousands of dollars in ocean freight to transport "trapped air."
Freight Cost Mitigation
A standard 40-foot High Cube (40HQ) container can hold approximately 80 to 100 flat, uncompressed full-size mattresses. By applying automated roll-pack compression technology, the same 40HQ container accommodates 350 to 500 units. This represents a 300% to 400% increase in payload efficiency, slashing freight costs per unit by up to 75%.
Hospitality & B2B Procurement
Large-scale commercial projects—such as 300-room hotel installations, university dormitories, and luxury apartment developments—require synchronized delivery schedules. Compressed vacuum packaging minimizes site staging space, allows rapid elevator transport, and reduces installation labor by over 60%.
Eco-Friendly Degradation & Circularity
Sustainability is moving from a marketing slogan to a strict regulatory baseline. Modern compressed mattresses engineered by top-tier manufacturers focus on mono-material design principles—allowing seamless separation of steel coils from textiles and memory foam for 100% recyclable end-of-life processing.
China Industry 4.0: Foshan Shunde Manufacturing Ecosystem
Located in Longjiang Town, Shunde District, Foshan City—the recognized furniture capital of the world—our manufacturing hub represents the apex of Industry 4.0 integration. The competitive advantage of China's premier compressed mattress cluster lies in complete supply chain verticality within a 15-kilometer operational radius.
Automated Wire Coiling
Swiss and Italian high-speed CNC pocket coil machines turn high-carbon steel wire into enclosed pocket springs at over 220 springs per minute with zero wire variance.
Continuous Foaming Line
Our 200-meter continuous chemical foaming line allows precise control over polyol/isocyanate ratios, producing consistent foam density throughout full production runs.
Intelligent Vacuum Roll-Packing
Automated industrial press machines apply up to 500kN of force while sealers use multi-track thermal impulse welds to ensure zero vacuum seal failures during sea transport.
In-Line Quality Assurance
Every single unit undergoes laser-guided dimension mapping, roll-pack pressure monitoring, and batch barcoding for total raw material traceability from factory floor to end retail store.
Localized Support, Global Compliance & Regulatory Assurance
Exporting mattresses to North America, Europe, Australia, and the Middle East requires strict adherence to localized fire safety and chemical safety mandates. Non-compliance can result in customs detentions, severe financial penalties, or complete product recalls. As an experienced B2B manufacturer, we guarantee full international compliance through third-party certified testing laboratories (SGS, Intertek, TUV).
US Flame Retardancy (CFR 1633 & 1632)
Our mattresses engineered for the US market incorporate non-toxic, chemical-free inherently fire-retardant (FR) barrier socks made of fiberglass-free silica ray-on or inherently flame-resistant aramid blends that easily pass 30-minute open flame burner tests.
UK & EU Fire Safety (BS 7177 / BS 5852)
For UK residential and commercial hospitality procurement, we utilize Crib 5 (Source 5) and Match & Cigarette resistant fabrics and foams, ensuring full compliance with British fire regulations without compromising tactile comfort.
Chemical & Emissions Safety
All polyurethane foams produced in our facilities are CertiPUR-US certified, guaranteeing zero ozone depleters, heavy metals, formaldehyde, or regulated phthalates. Ticking textiles comply with OEKO-TEX Standard 100 Class I standards.
Customs Clearance & Tariff Support
Navigating global tariffs requires flexible origin logistics. We assist clients with complete Certificate of Origin (Form E, Form F, CO) documentation, DDP (Delivered Duty Paid) door-to-door delivery logistics, and anti-dumping mitigation strategies.
Global Enterprise Procurement Demands & Customization
Modern B2B importers rarely purchase off-the-shelf standardized products. Success in competitive local markets demands custom OEM/ODM development tailored to specific demographic preferences, firmness levels, and retail branding requirements.
End-to-End OEM/ODM Customization Matrix
From private label box design to specialized firmness zoning, our engineering team acts as your dedicated offshore R&D department:
- Zoned Ergonomic Support: 3-zone, 5-zone, or 7-zone pocket coil configurations utilizing varied wire gauges (1.8mm to 2.3mm) to support shoulder, lumbar, and leg regions.
- Advanced Cover Textiles: Cooling PCM (Phase Change Material) covers, bamboo charcoal fibers, anti-dust mite copper-infused threads, and organic cotton jacquards.
- Custom Packaging & Branding: Full-color private label box printing, customized instruction manuals, branded unboxing tools, and custom sewn woven labels.
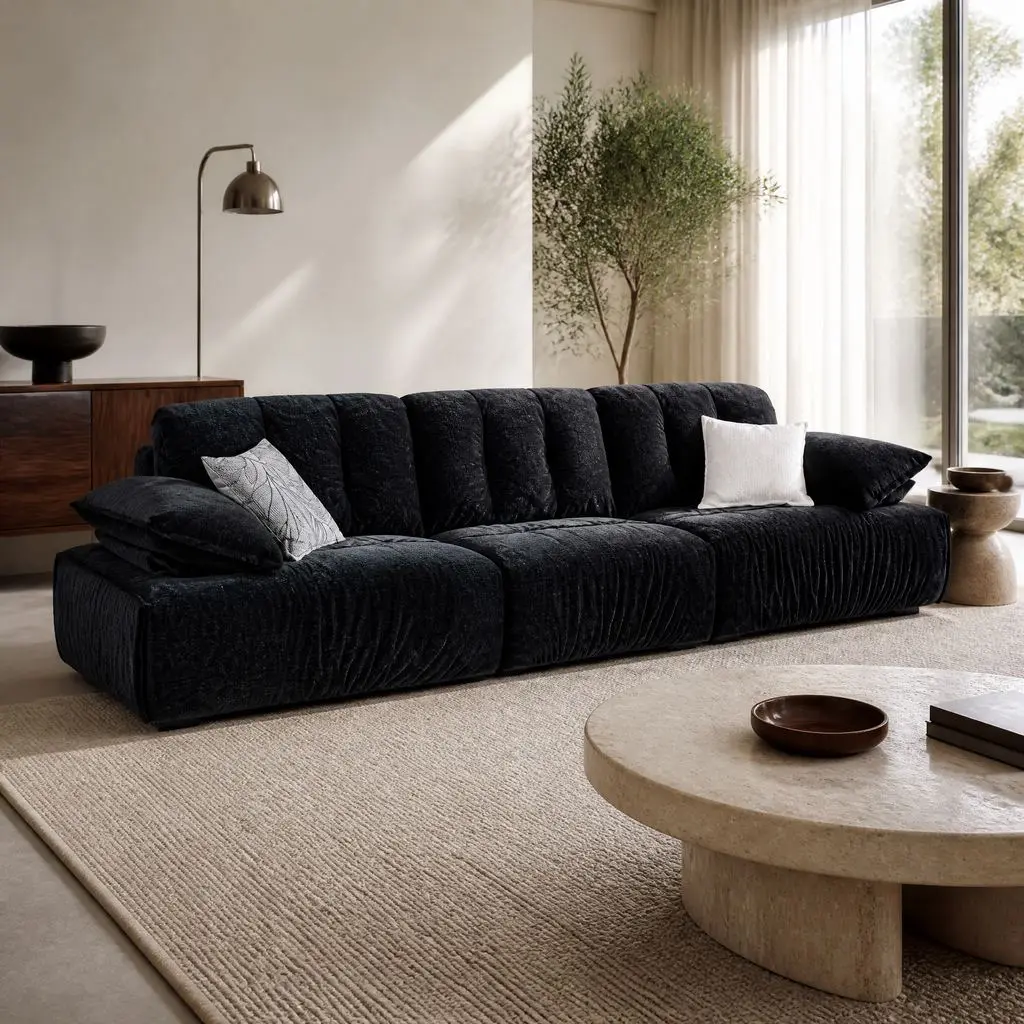
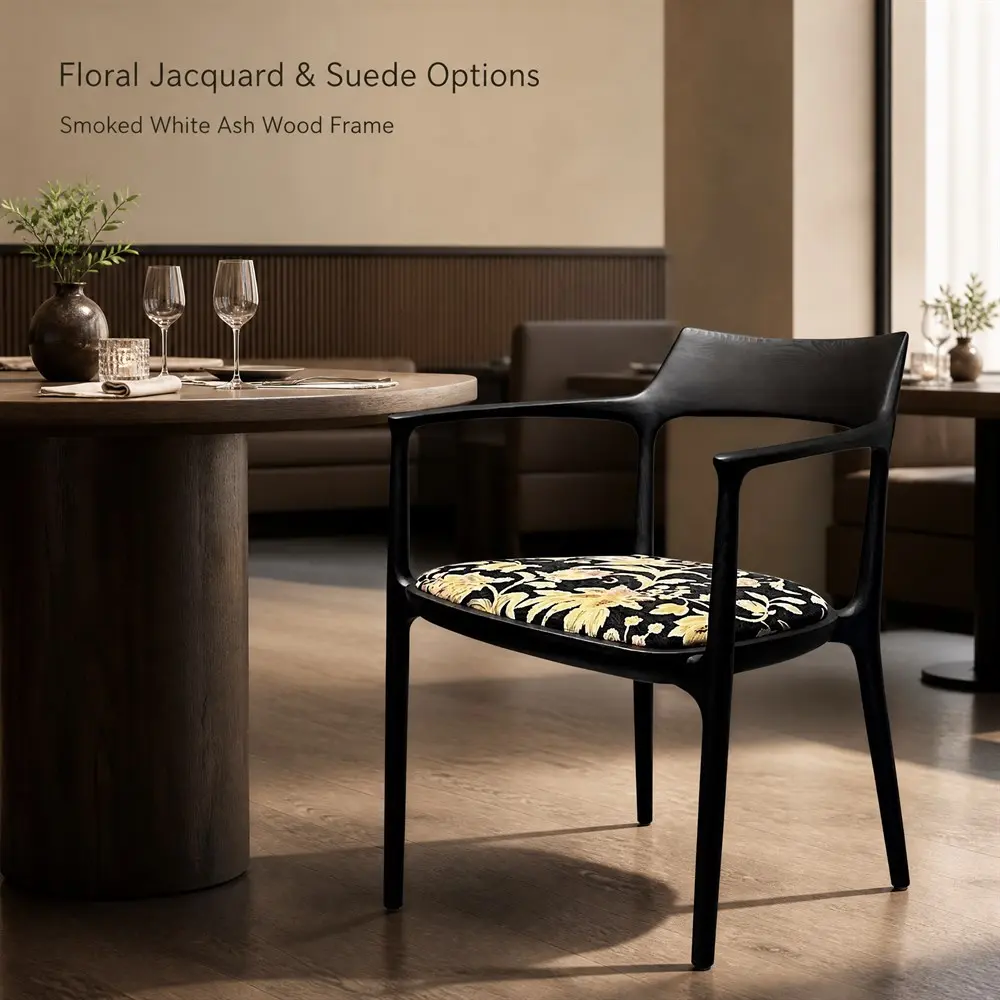
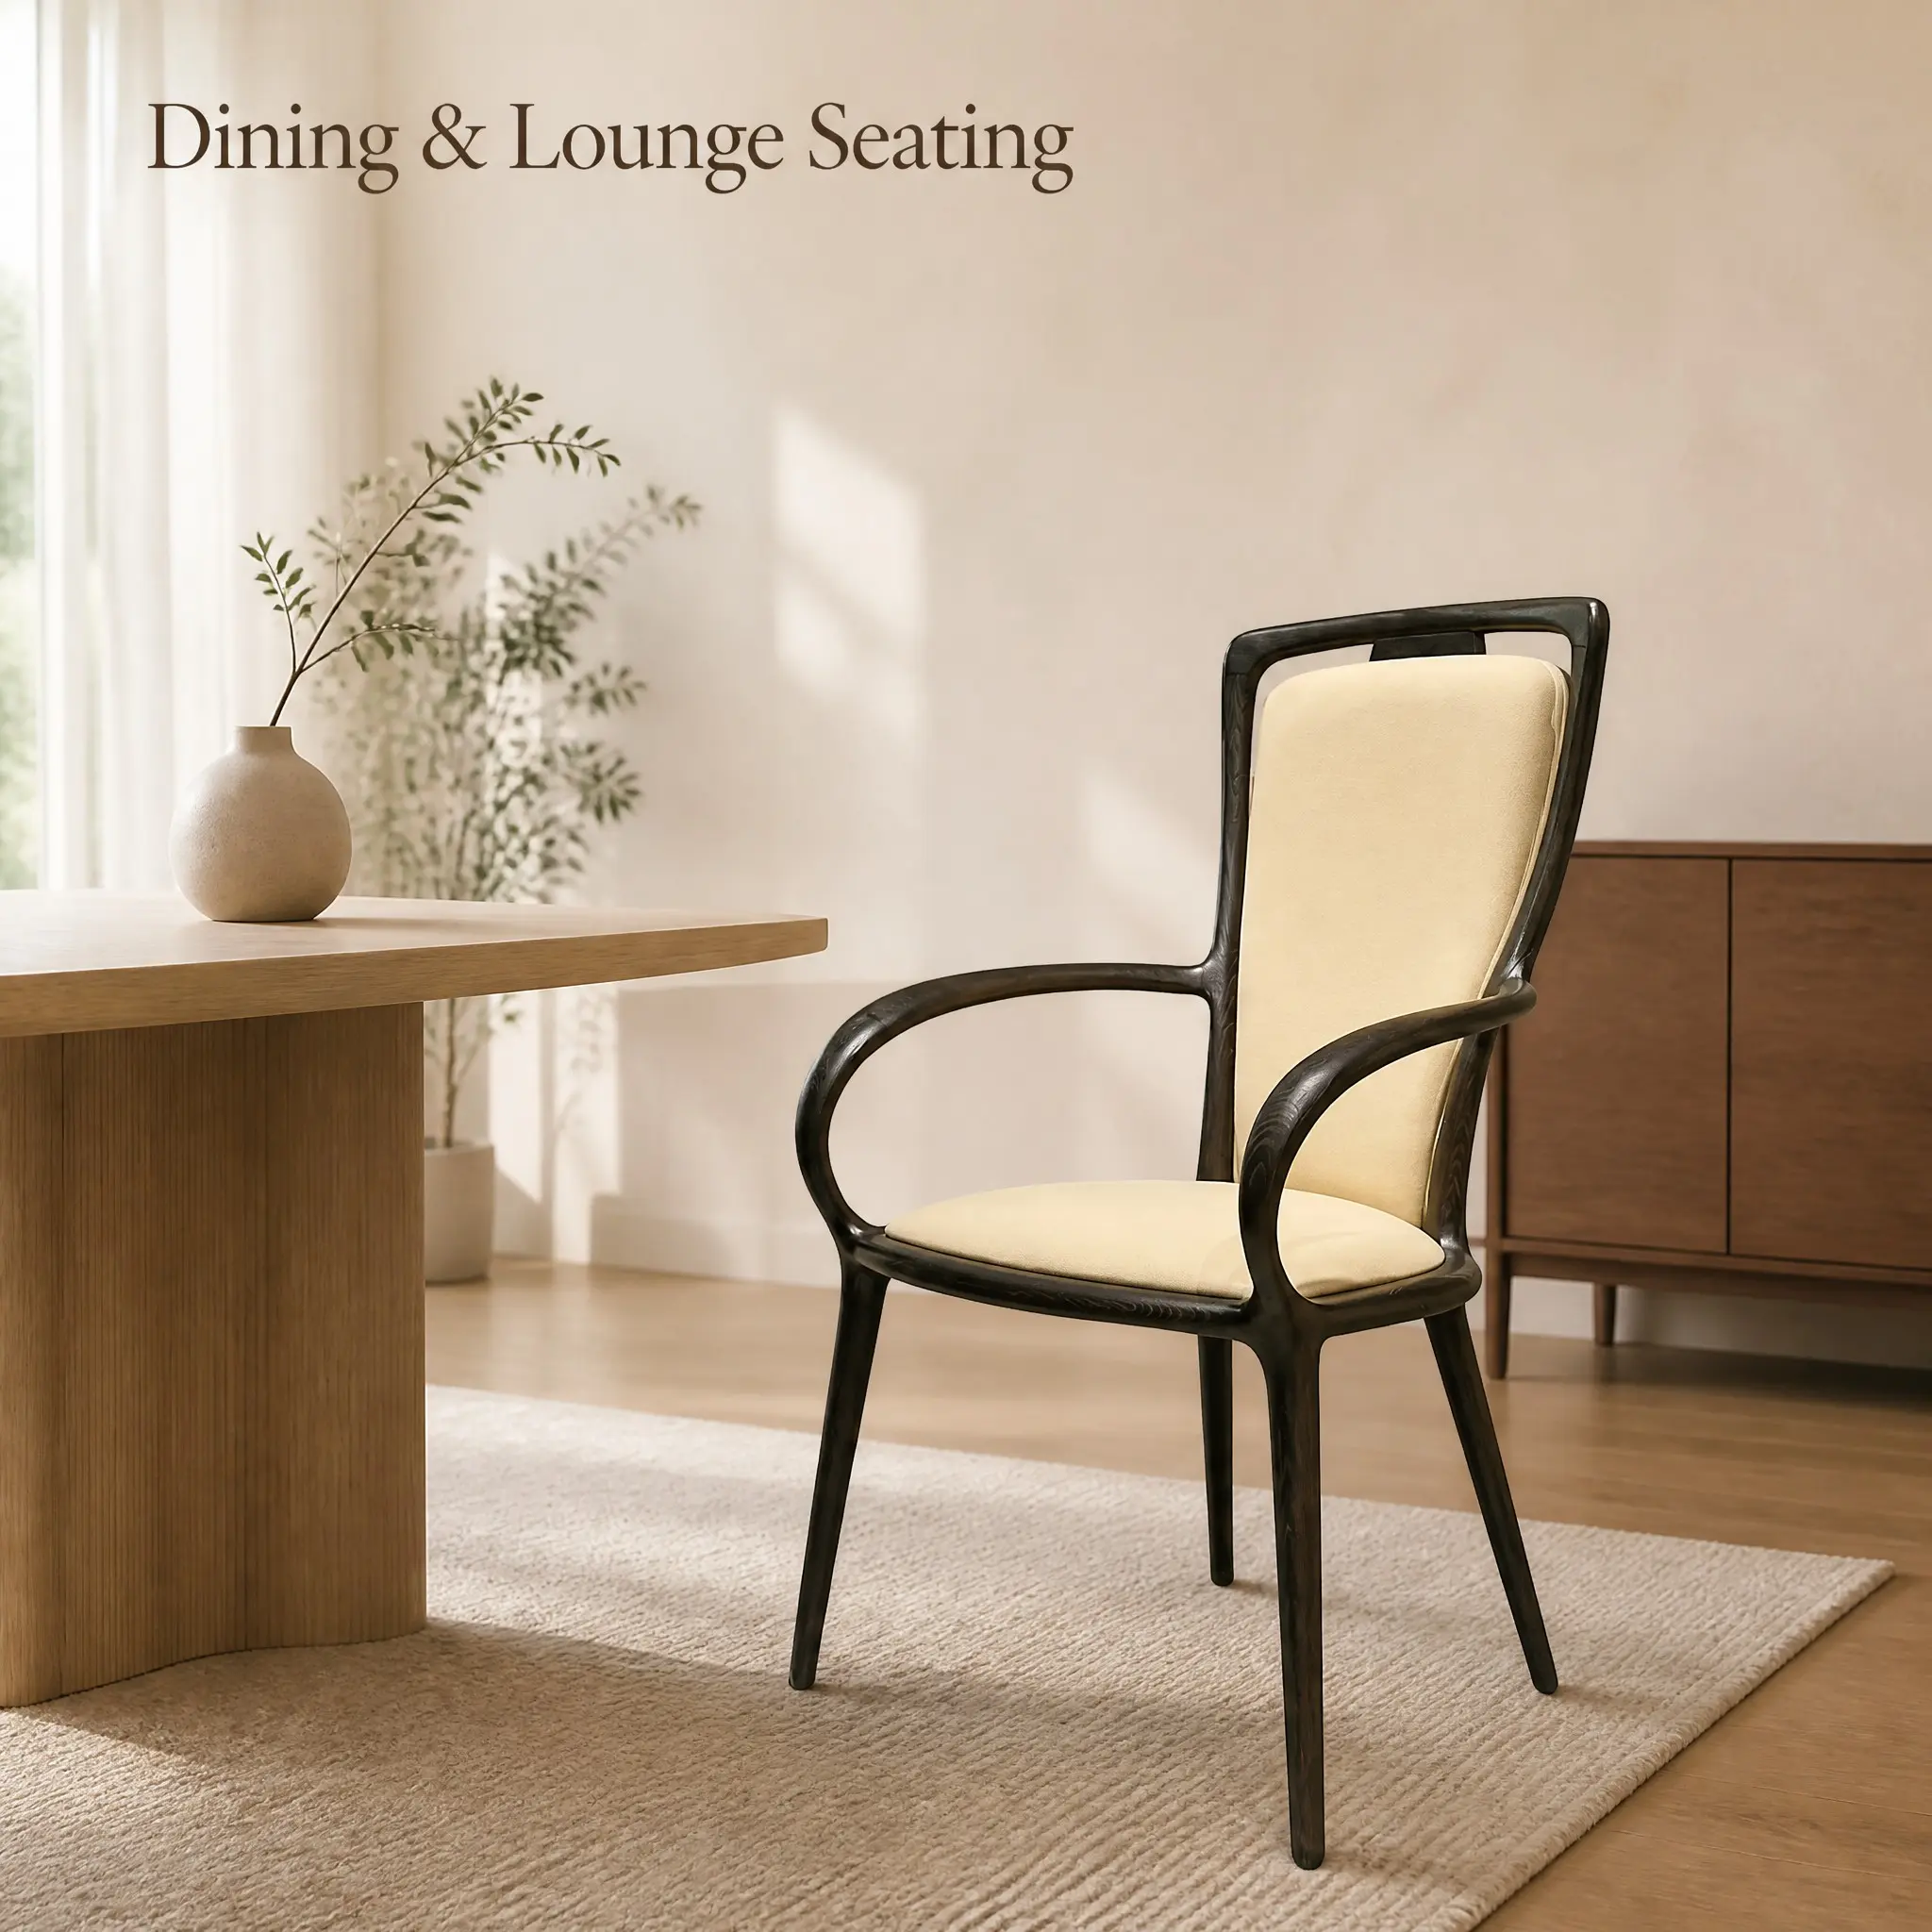
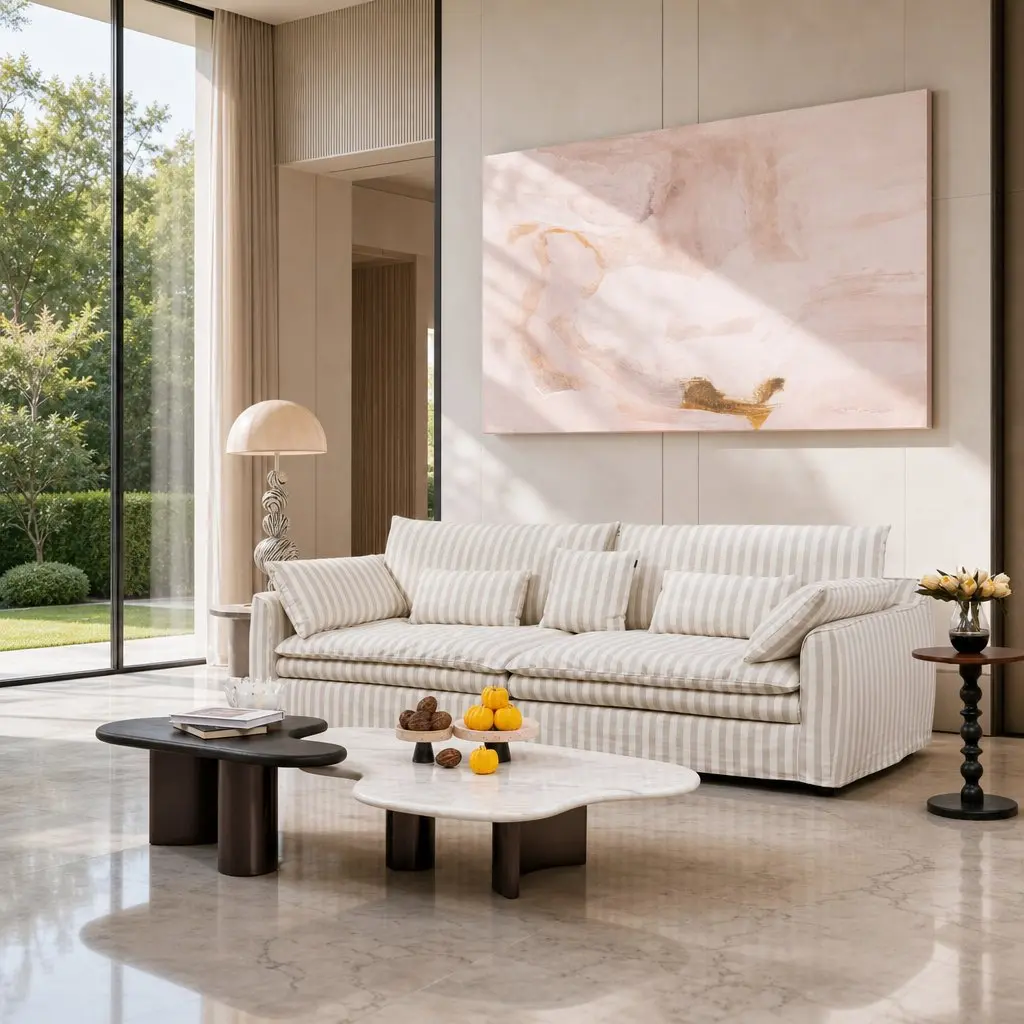
- Multi-Category Container Consolidation: Mix mattresses with upholstered bed frames, dining chairs, and living room seating inside a single container to optimize inventory turnover.
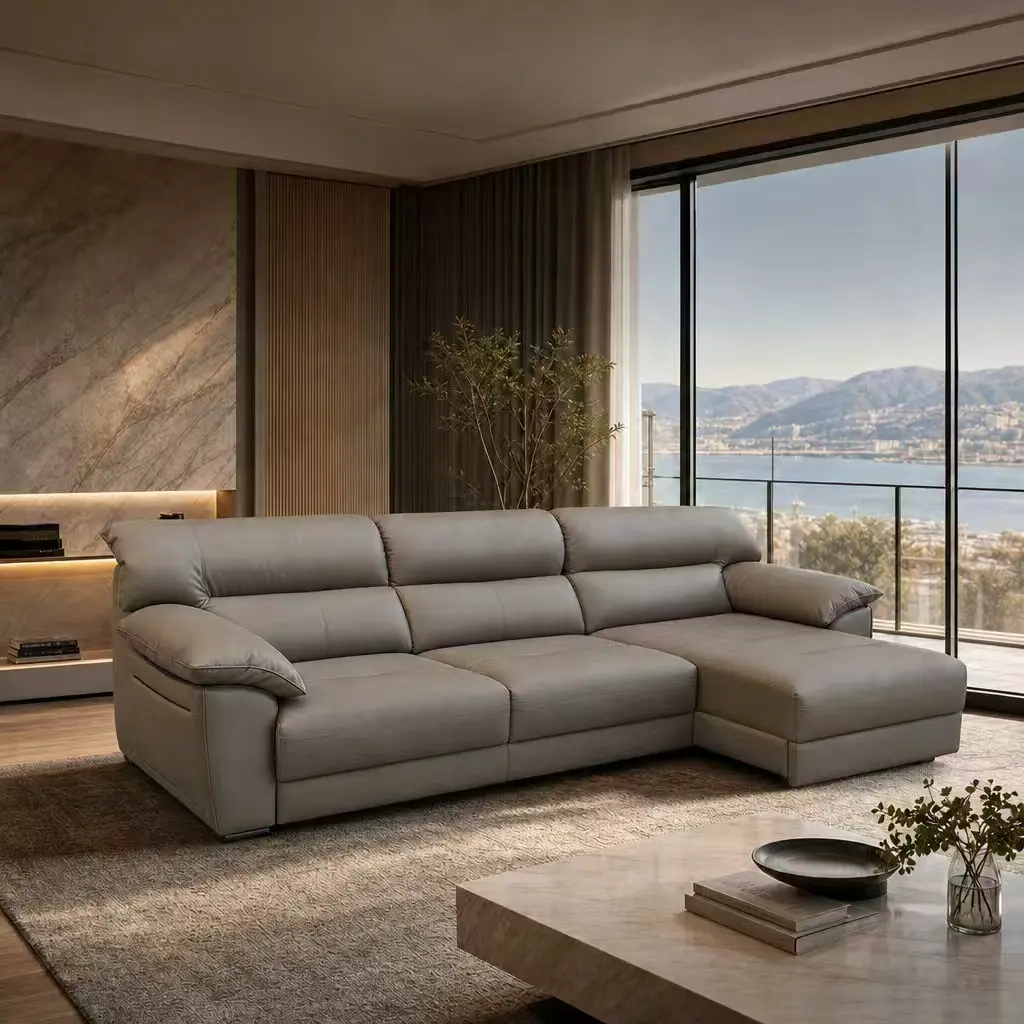
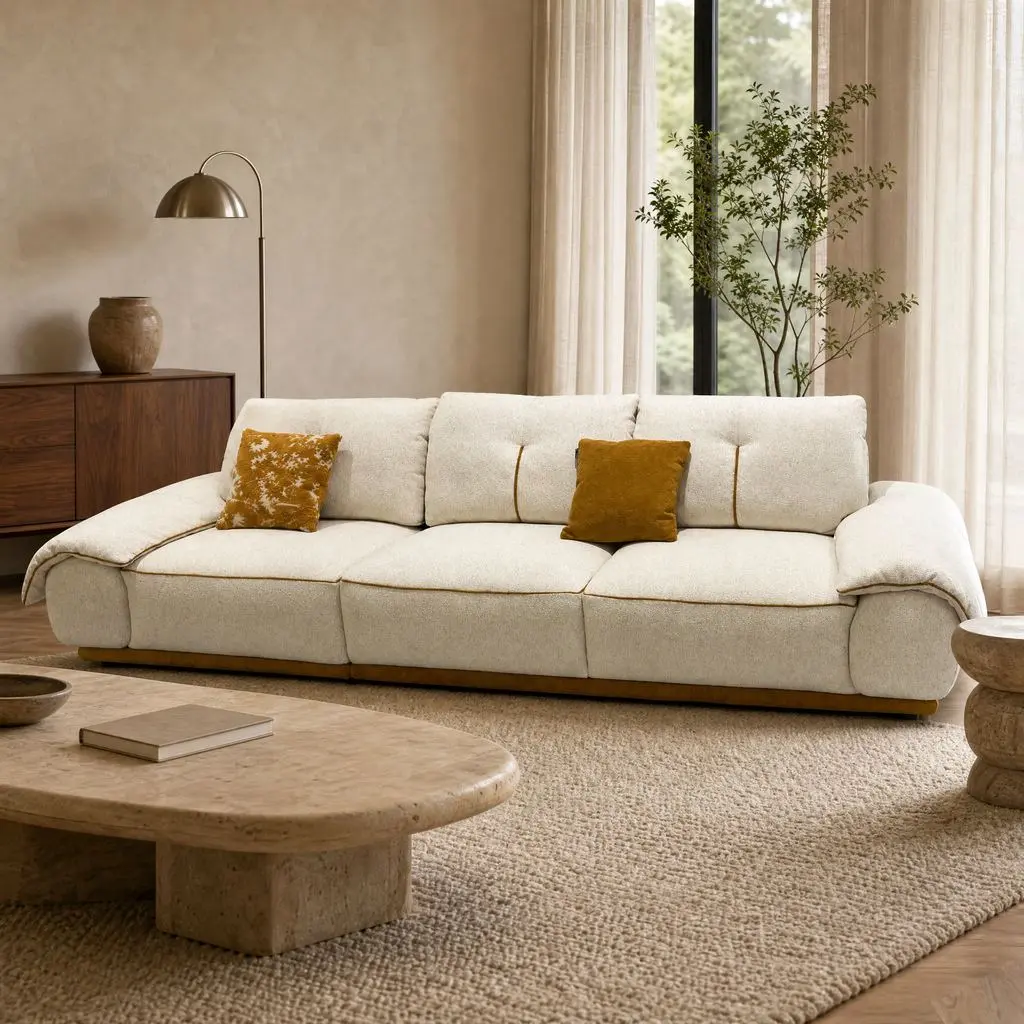
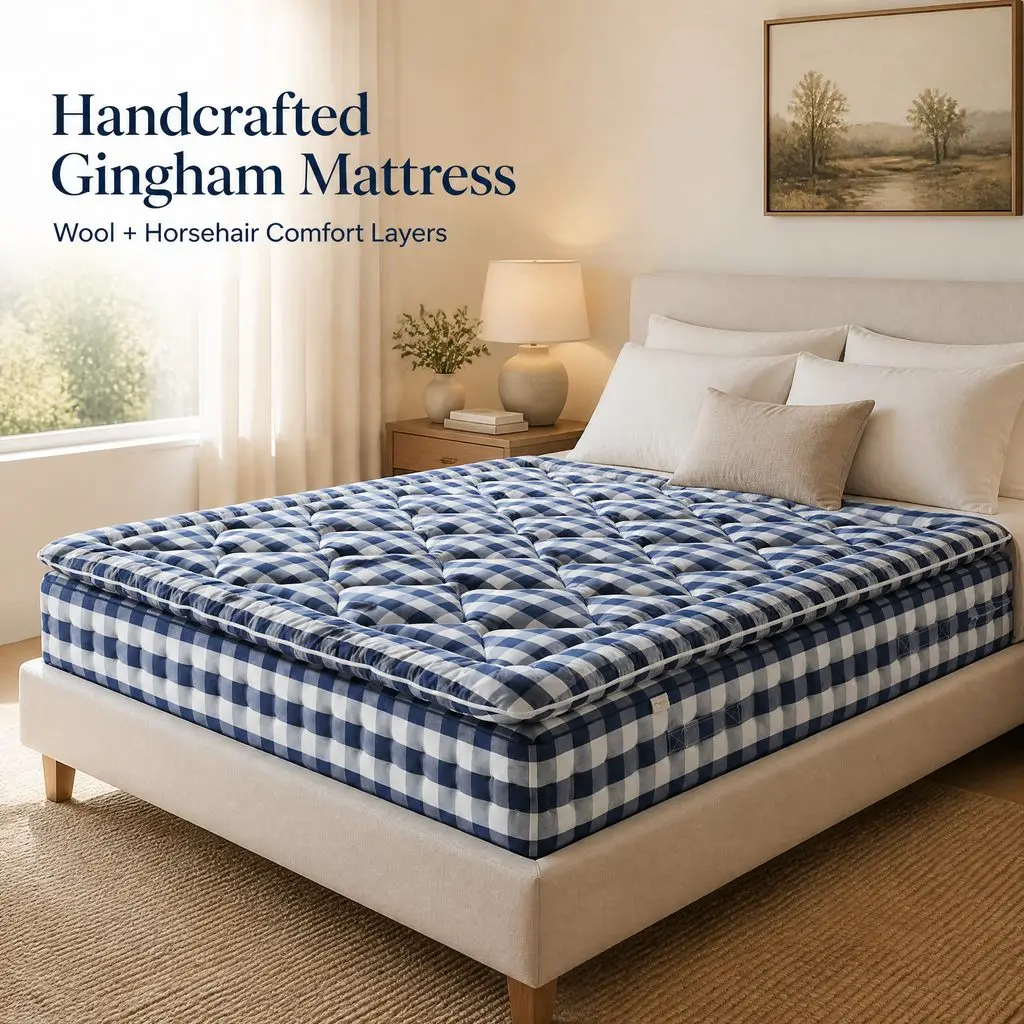
Featured OEM Export Collections (Part II)
Discover our complete whole-house and commercial hospitality product ecosystem available for consolidated enterprise shipping.
Deep-Dive B2B Technical Q&A
Answers to the most critical technical, logistical, and commercial inquiries raised by international mattress wholesalers, importers, and procurement directors.